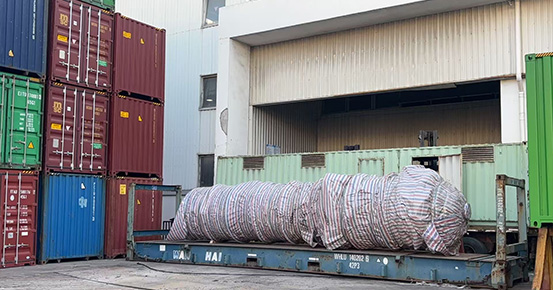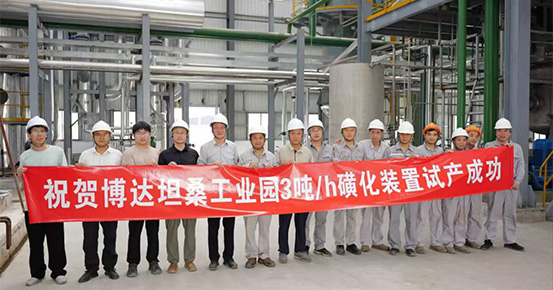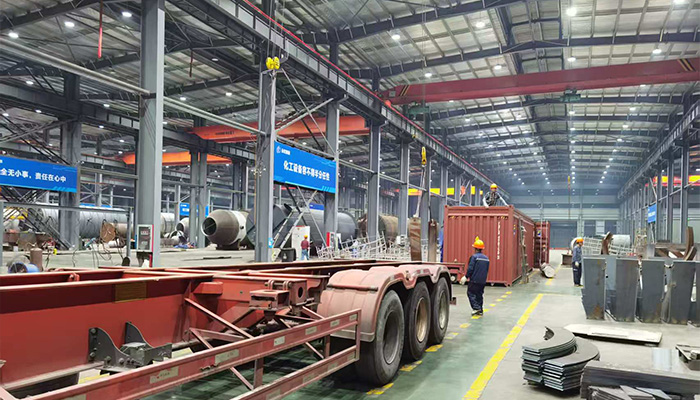
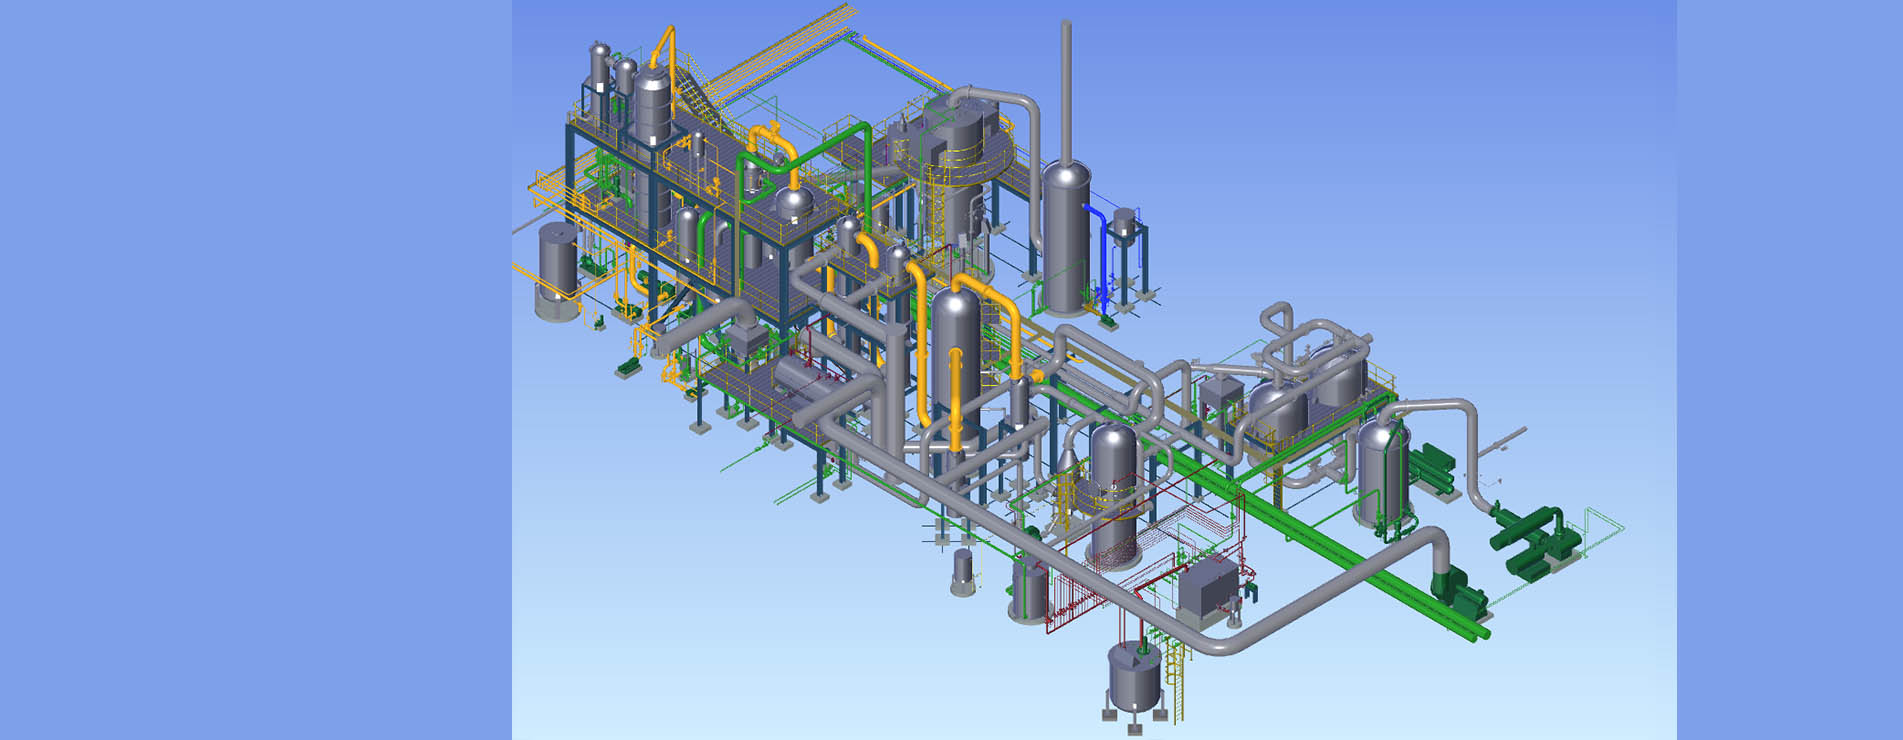
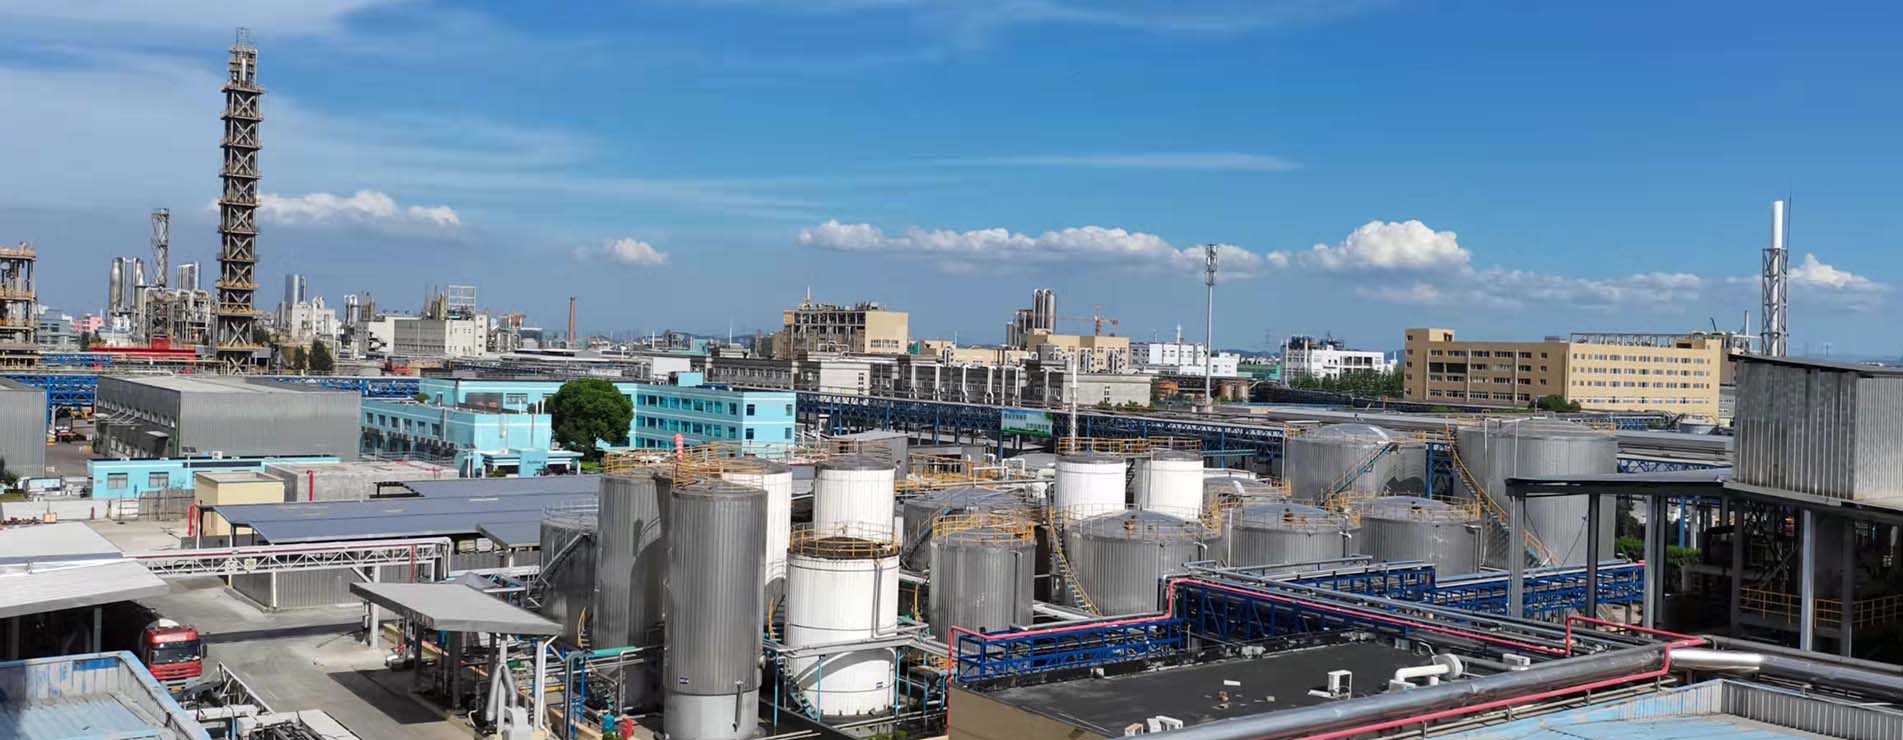
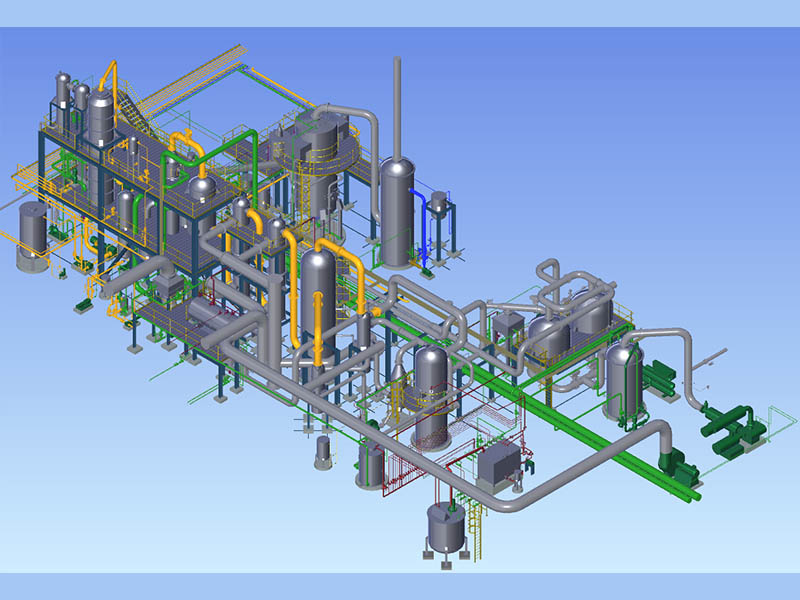
WEIXIAN sulphonation/sulfonation plants represent the highest level in the industry. So far, we can provide from a one-tube pilot plant to 10t/h mass production plant. Among 200+ projects we have done, the majority of them were turnkey basis, including but not limited to:
· LABSA (sulfonic acid) production line
· SLES production line
· SLS production line
· AOS production line
· HABSA production line
· MES production line
· SLS/AOS/sulfonic acid sodium salt drying units
· Other anionic surfactant production lines
By adopting state-of-the-art designs and processes, all the performance aspects including plant reliability, finished product qualities, and unit raw material/power consumption are superior to that of competitive plants.
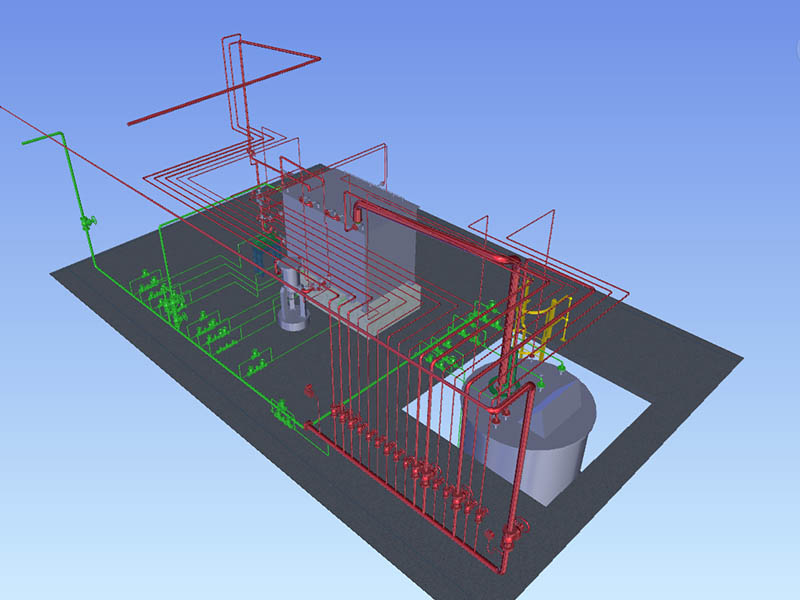
Liquid or solid sulfur is fed into pipelines insulated with steam coils and jackets, then delivered to the sulfur melting tank. The molten sulfur is subsequently pumped to the high-level tank and further conveyed to the sulfur burner by a submerged gear pump or a gear pump with steam-jacket insulation. By integrating a mass flow meter with a variable-frequency drive (VFD) on the gear pump, the flow rate of liquid sulfur is maintained at a stable and controlled rate.
Features: The WEIXIAN liquid sulfur gear pump resists clogging by impurities. With the flow rate regulated by a mass flow meter and VFD, delivery is stable and accurate. The system also enables online monitoring of operating parameters, offering maximum convenience for controlling SO₃ concentration, adjusting plant performance, and switching product grades.
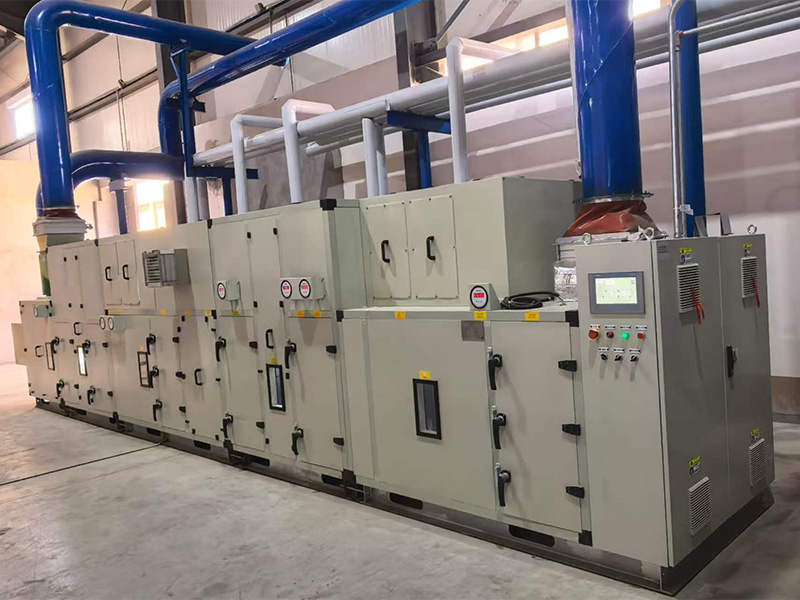
The Problem with Conventional Drying: Traditional dual tank drying systems cycle between adsorption and regeneration every eight hours – causing flow and temperature swings, dew point drift, valve wear, and constant operator attention.
WEIXIAN's Answer: Unit 22. A single, continuously rotating silica gel bed that eliminates switching entirely. A World First from WEIXIAN.
Key Advantages
Atmospheric air is compressed by the main blower and fed to a dehumidifier, where most of the moisture is removed by water cooling and refrigeration. The air then passes through a silica gel bed for deep dehumidification, ultimately producing dry air with a dew point of −60 °C. The flow rate of dry air (Nm³/h or kg/h) is regulated by the speed of the main blower, which is controlled in closed loop by an orifice flow meter and the blower's variable-frequency drive (VFD).
Features: The air-cooling finned heat exchanger uses SS304 stainless steel for both fins and tubes, delivering a service life far longer than that of conventional copper-tube/aluminum-fin construction.
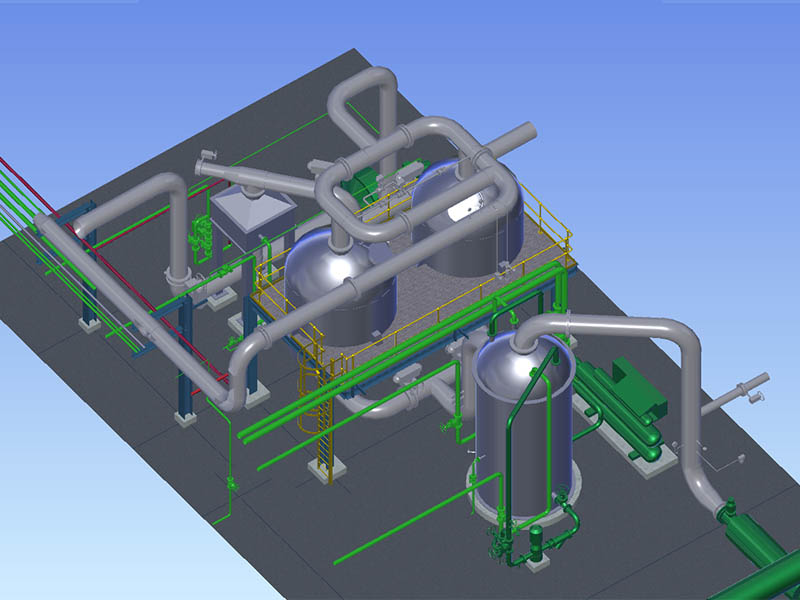
Liquid sulfur is precisely metered and fed to the sulfur burner, where it fully combusts with dry air to generate SO₂. After cooling, the SO₂ gas enters the converter and is converted to SO₃ over a vanadium catalyst. Following further cooling, the SO₃ gas is sent to the sulphonation/sulfation unit. The SO₂ and SO₃ gases are cooled by cooling air in a tube-type heat exchanger; the resulting hot air is collected and routed to the waste heat recovery unit to generate steam and hot water. The secondary hot air is then used for silica gel regeneration and for the evaporation and crystallization of scrubber wastewater in Unit 38.
Features: The SO₂ cooler adopts inlet-end insulation protection and a floating-tube design, which prevents intergranular corrosion of the stainless steel above 600 °C and doubles the service life. By integrating the start-up pre-heater with the waste heat recovery unit, the steam produced during converter preheating is also used for sulfur melting and hot-water generation, so that WEIXIAN plants require no external steam.
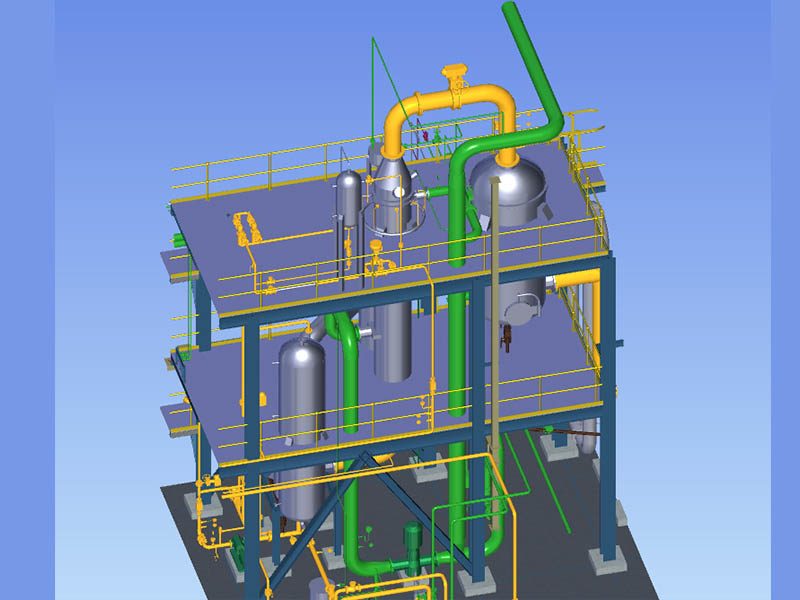
SO₃ gas, adjusted to a precise concentration (%), passes through an SO₃ filter and then reacts with the organic raw material in the reactor. The heat of reaction is removed by circulating cooling water on the shell side of the reactor. The exhaust gas passes through a gas–liquid separator and a cyclone separator before entering the exhaust-gas treatment unit, while the organic acid is sent to an aging and stabilization unit, or to a neutralization and dioxane-stripping unit.
The flow rate of the organic raw material is controlled by a mass flow meter and a control valve (or by the VFD of a gear pump). The liquid level in the gas–liquid separator is controlled by a level transmitter and the VFD of the discharge pump. The flow rate and density of the organic acid are measured by a mass flow meter, with density under cascade control to trim the raw-material flow rate. The inlet temperature of the circulating cooling water is held constant by makeup water, and the cooling-water flow is regulated by a control valve whose opening depends on the reactor temperature difference on each pass.
Features: WEIXIAN incorporates more than three key design improvements to enhance reactor reliability. The dimensions of every reactor tube, distributor and nozzle are manufactured to a high degree of uniformity. Each reactor tube is produced by high-precision rolling followed by an oxygen-free annealing process, so that the surface finish is uniform across all tubes and along the length of each tube. Compared with competing technologies, WEIXIAN plants deliver longer continuous operating runs and lower dioxane levels when producing SLES.
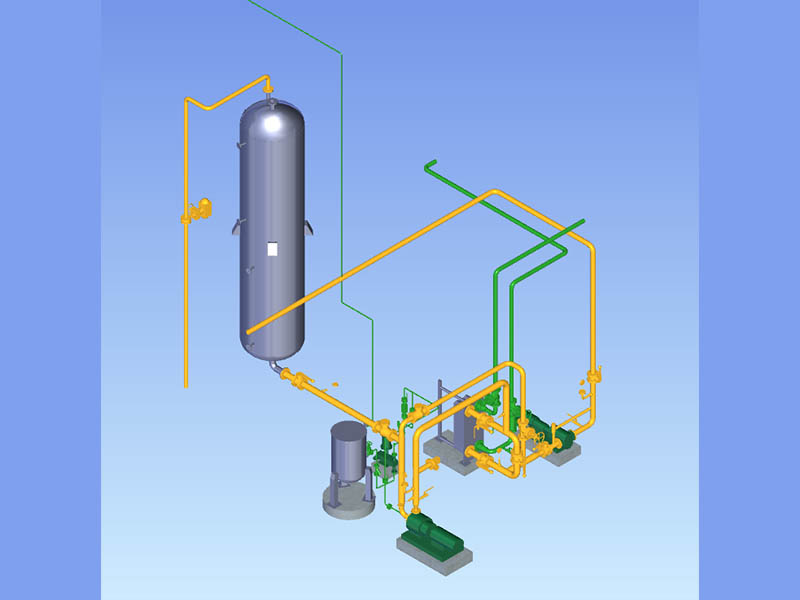
The LABSA (linear alkylbenzene sulphonic acid) from the separator is fed to the aging vessel by the first discharge pump, then stabilized with water in the stabilization pump. After cooling, the LABSA is pumped to the finished-product tanks by the second discharge pump. The liquid level in the aging vessel is controlled by a level transmitter and the VFD of the second discharge pump.
Features: The WEIXIAN aging vessel is of vertical, static-mixing construction with no back-mixing, and the aging time is precisely controlled. This brings the aging conversion rate close to its theoretical limit, minimizes the free-oil and free-sulfuric-acid content, and correspondingly raises the active-matter content to or toward 98%.
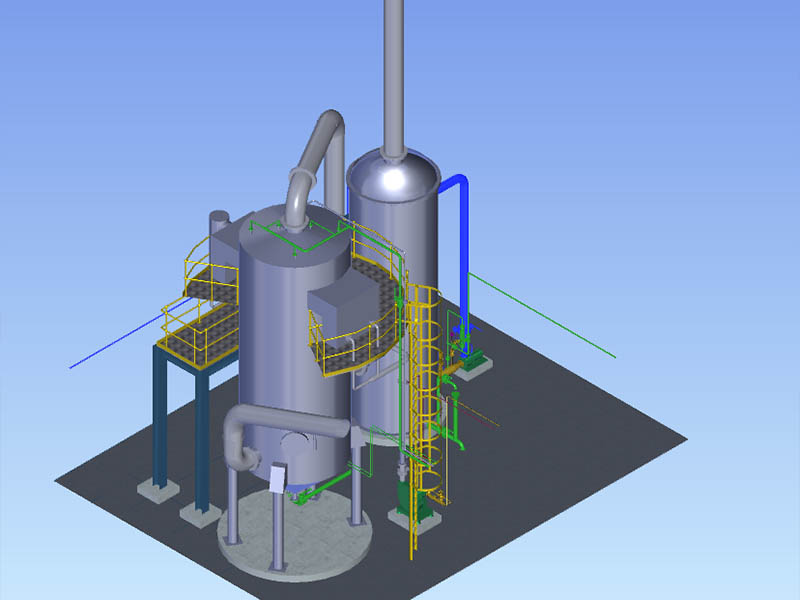
Before discharge, the exhaust gas is treated to remove organic acid mist and SO₃ in an electrostatic precipitator (ESP), while SO₂ is removed in a scrubber.
Features: WEIXIAN uses plate-type tubes as the ESP cathode. Compared with steel-wire cathodes, this design requires no maintenance.
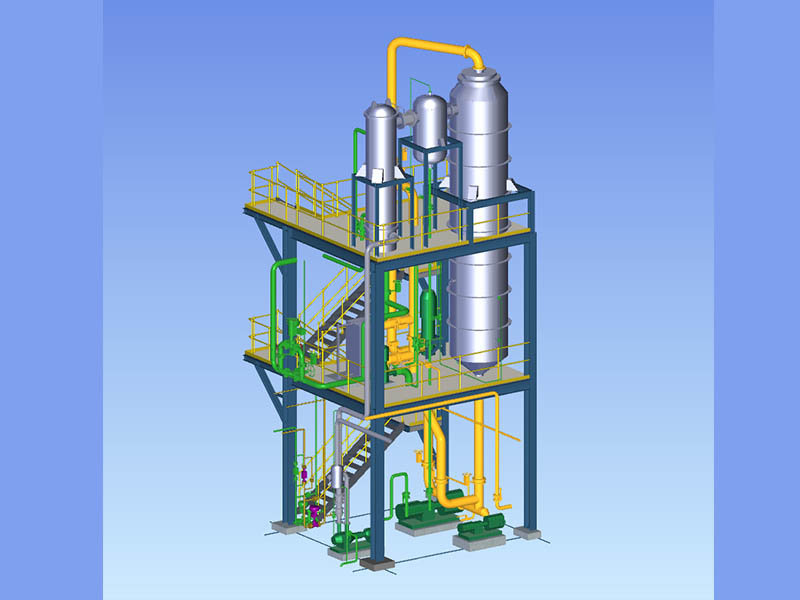
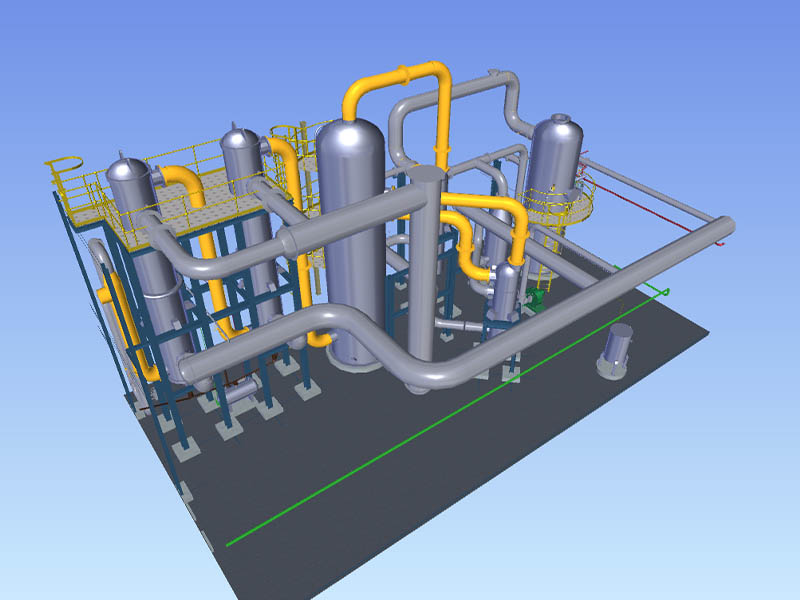
When producing SLES, the sulfate is neutralized with pure water, caustic soda, hydrogen peroxide (H₂O₂) and a buffer in the neutralization reactor, where all ingredients are brought to reaction by high-shear mixing. Dioxane is then stripped out together with air in the stripping tower under vacuum, while cooling is also carried out in the same tower.
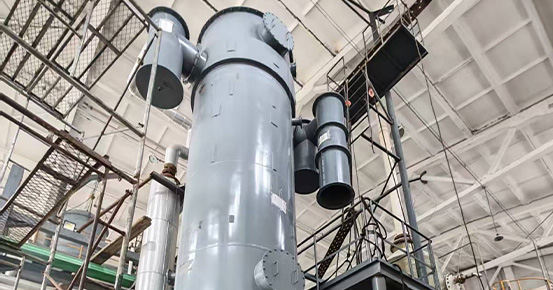
Features: Compared with other vacuum-neutralization process, the WEIXIAN stripping tower is a static unit with no motor and requires no maintenance. The product is reacted in a micro-positive-pressure reactor before entering the stripping tower, so that no acid-gas corrosion occurs in the condensate or the vacuum pump. The unit also incorporates a ten-times SLES recycle loop. Compared with similar technologies from other suppliers, this process keeps the neutralization temperature rise below 5 °C, yielding products with a lighter color, a more stable pH and lower dioxane content. The unit can achieve ultra-low dioxane levels.
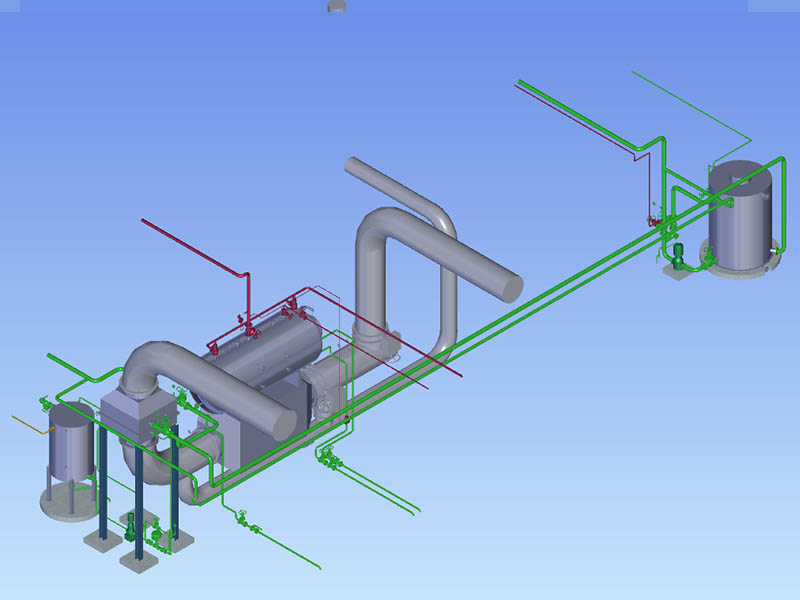
The hot air first enters the heat-pipe exchanger, where heat is transferred to the soft water inside, generating steam at 0.4–0.6 MPa. After leaving the heat-pipe exchanger, the hot air is further used to pre-heat the reverse-osmosis (R/O) water and produce hot water.
Features: With the waste heat recovery system, the plant requires no external steam for cold start-up. During normal operation, the plant achieves full steam and hot-water self-sufficiency.
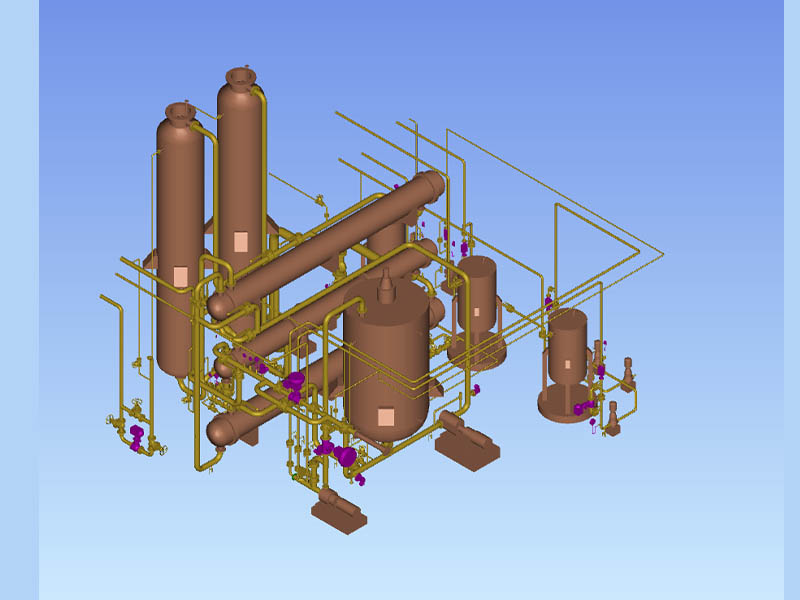
The sulfolactone hydrolysis system consists of a boosting pump, three heat exchangers and a hydrolyzer. After aging, the α-olefin sulfonate is fed, together with pure water, caustic soda, hydrogen peroxide solution and buffer, into the neutralization reactor. Following high-shear mixing, the mixture is pumped through two heat exchangers and the hydrolyzer in sequence; after hydrolysis, the finished product AOS is obtained.
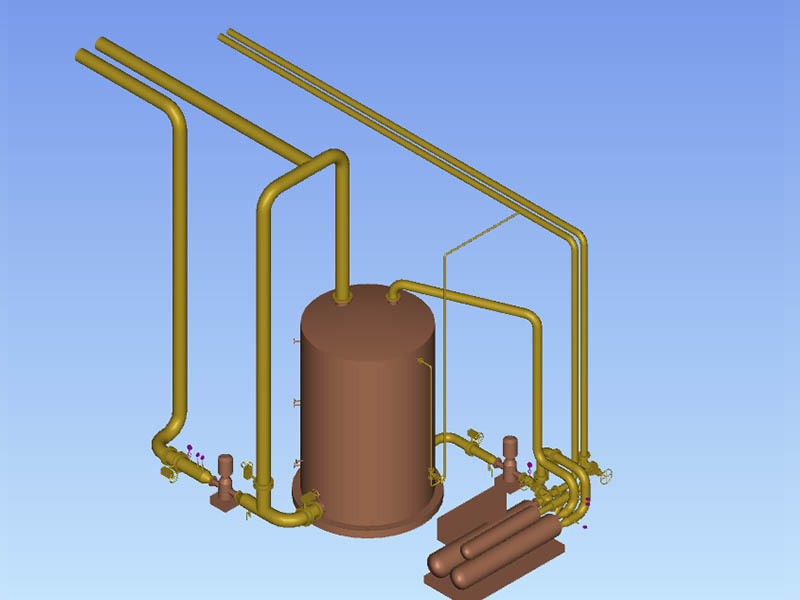
When AOS is produced, the temperatures at the top of the sulfonation reactor, aging vessel and α-olefin inlet need to be decreased to ensure product stability. A chilling water unit is required. The chilling water unit consists of a chilling water group, chilling water tank, and two circulating pumps. One circulating pump transports the water to the chilling group, decreasing the temperature to the set point, then backflow to chilling water tank; the other circulating pump transports the chilled water to the user, then backflow to chilling water tank.
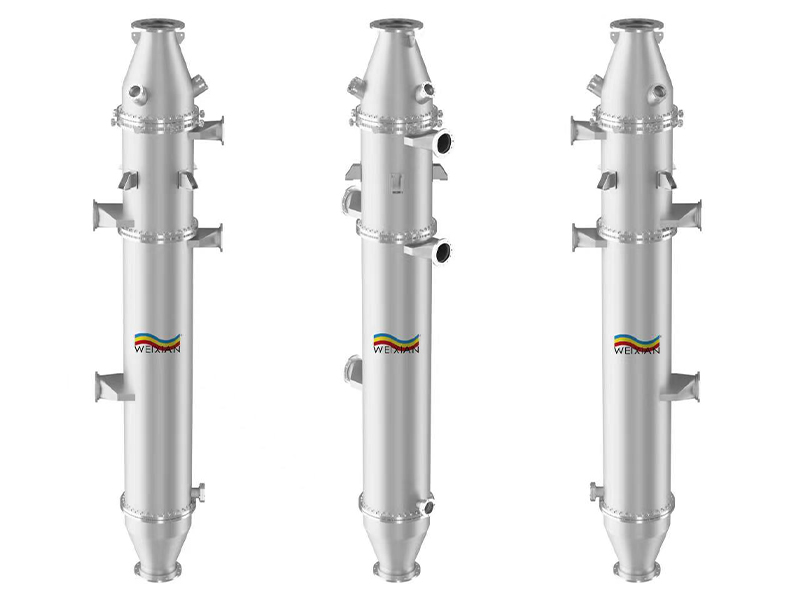
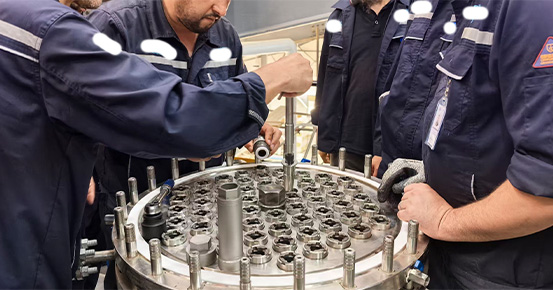
WEIXIAN adopts multi-tube falling film reactor. Its capacity ranges from single-tube configuration up to a 240-tube unit (10 t/h). Since 1995, WEIXIAN has delivered hundreds of reactors, among which more than 40 units feature a capacity exceeding 5 t/h. By 2026, WEIXIAN had successfully commissioned six set of 7.5 or 8t/h reactors.
1. Organic feed distribution system at reactor head
After calibration, flow deviation is controlled within ±1.5%. The distribution header and nozzles are machined and formed in a single clamping setup via CNC machining. Critical dimensional tolerances are guaranteed at ±0.005 mm, with secondary dimensions held to ±0.01 mm.
2. Surface finish of reaction tube inner bore
Reaction tubes are manufactured by high-precision cold rolling followed by annealing, and treated under vacuum at 1040 °C to eliminate intermolecular residual stress. These processes yield an internal and external surface finish of Ra 0.4 (mirror-like) for each tube; the inner and outer diameter deviation of reaction tubes is limited to less than ±0.02 mm.
3. Welding and non-destructive inspection for distribution header and reaction tubes
The joint between distribution header and reaction tube employs high-frequency welding combined with GTAW (gas tungsten arc welding, argon arc welding), with fillet weld geometry. Non-destructive testing (NDT) is adopted for flaw detection. Every individual tube undergoes a 0.6 MPa hydrostatic pressure test and endoscopic inspection to verify weld integrity and internal tube dimensional accuracy.
4. Concentricity of the three tube sheets
All three tube sheets are machined on a machining center using a unified coordinate system. Tube concentricity tolerance is ±0.01 mm. The three tube sheets are stacked and secured in their assembly orientation, then every hole is checked one by one using an inspection mandrel to confirm concentricity deviation ≤ ±0.01 mm.
5. Sealing reliability
5.1 Cooling water seal between upper shell section and middle/lower shell sections
Cooling water flows into the second and third shell sections and discharges from the third section of the sulfonator. The first (upper) section is strictly isolated to maintain a separate circulation of 15 °C chilled water. This is critical to superior product quality, particularly for AOS production.
5.2 Bidirectional sealing for SO₃ and organic feed at the sulfonator upper section
On the first tube sheet, the compression screw assembly uses a composite screw head plus triple combined gaskets to form robust bidirectional sealing. It achieves complete isolation from oleum and prevents corrosion and leakage.
5.3 Cooling water sealing between distribution header and shell side
An innovative sealing structure significantly improves shell-side pressure resistance. The shell-side test pressure exceeds 0.6 MPa, permitting pressurized water return. All sealing elements are special fluororubber O-rings, delivering 100% sealing performance with lifetime maintenance-free operation.
5.4 Cooling water sealing at the lower reaction tube and shell side
Fluororubber O-rings are implemented here, providing 100% sealing performance and lifetime maintenance-free operation.
6. Additional technical advantages of WEIXIAN sulfonator
6.1 Extended operating campaign: Continuous LABSA production campaign ≥40 days
6.2 Continuous production campaign for 70% SLES exceeds 3 months
6.3 Continuous production campaign for AOS ≥25 days
6.4 Convenient sulfonator calibration Flow deviation at initial start-up can be controlled within ±1.5%. Replacement gaskets are available in thicknesses of 1.8–2.2 mm (standard thickness: 2 mm). This ensures premium product quality and extends sulfonator cleaning intervals.
6.5 Production turndown flexibility
LABSA capacity adjustment range: 55%–115%
70% SLES capacity adjustment range: 80%–140%
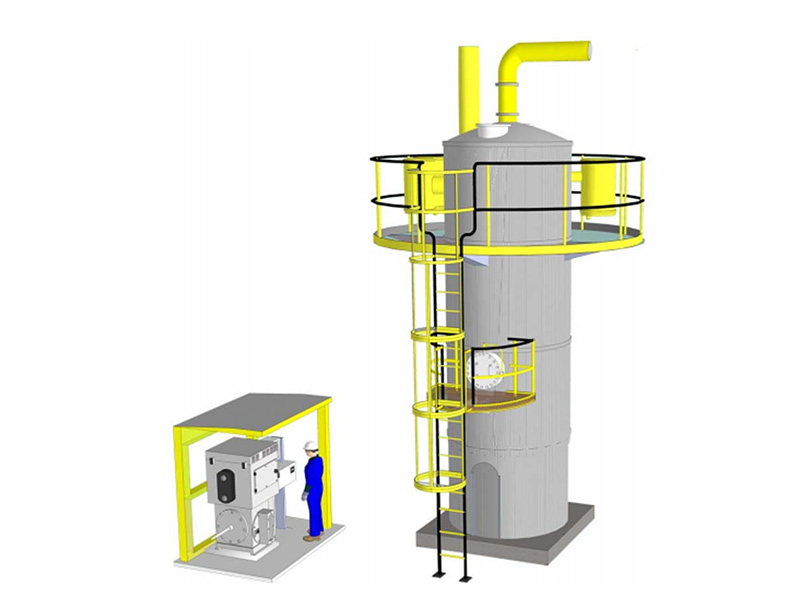
It adopts the cathode plate hollow-out design to avoid “black acid” accumulation. Cathode SS wires are replaced by SS tubes, in order to eliminate the risk of breaking.
The working voltage is 40,000 V, featured in excellent SO3 and organic acid mists removal performance.
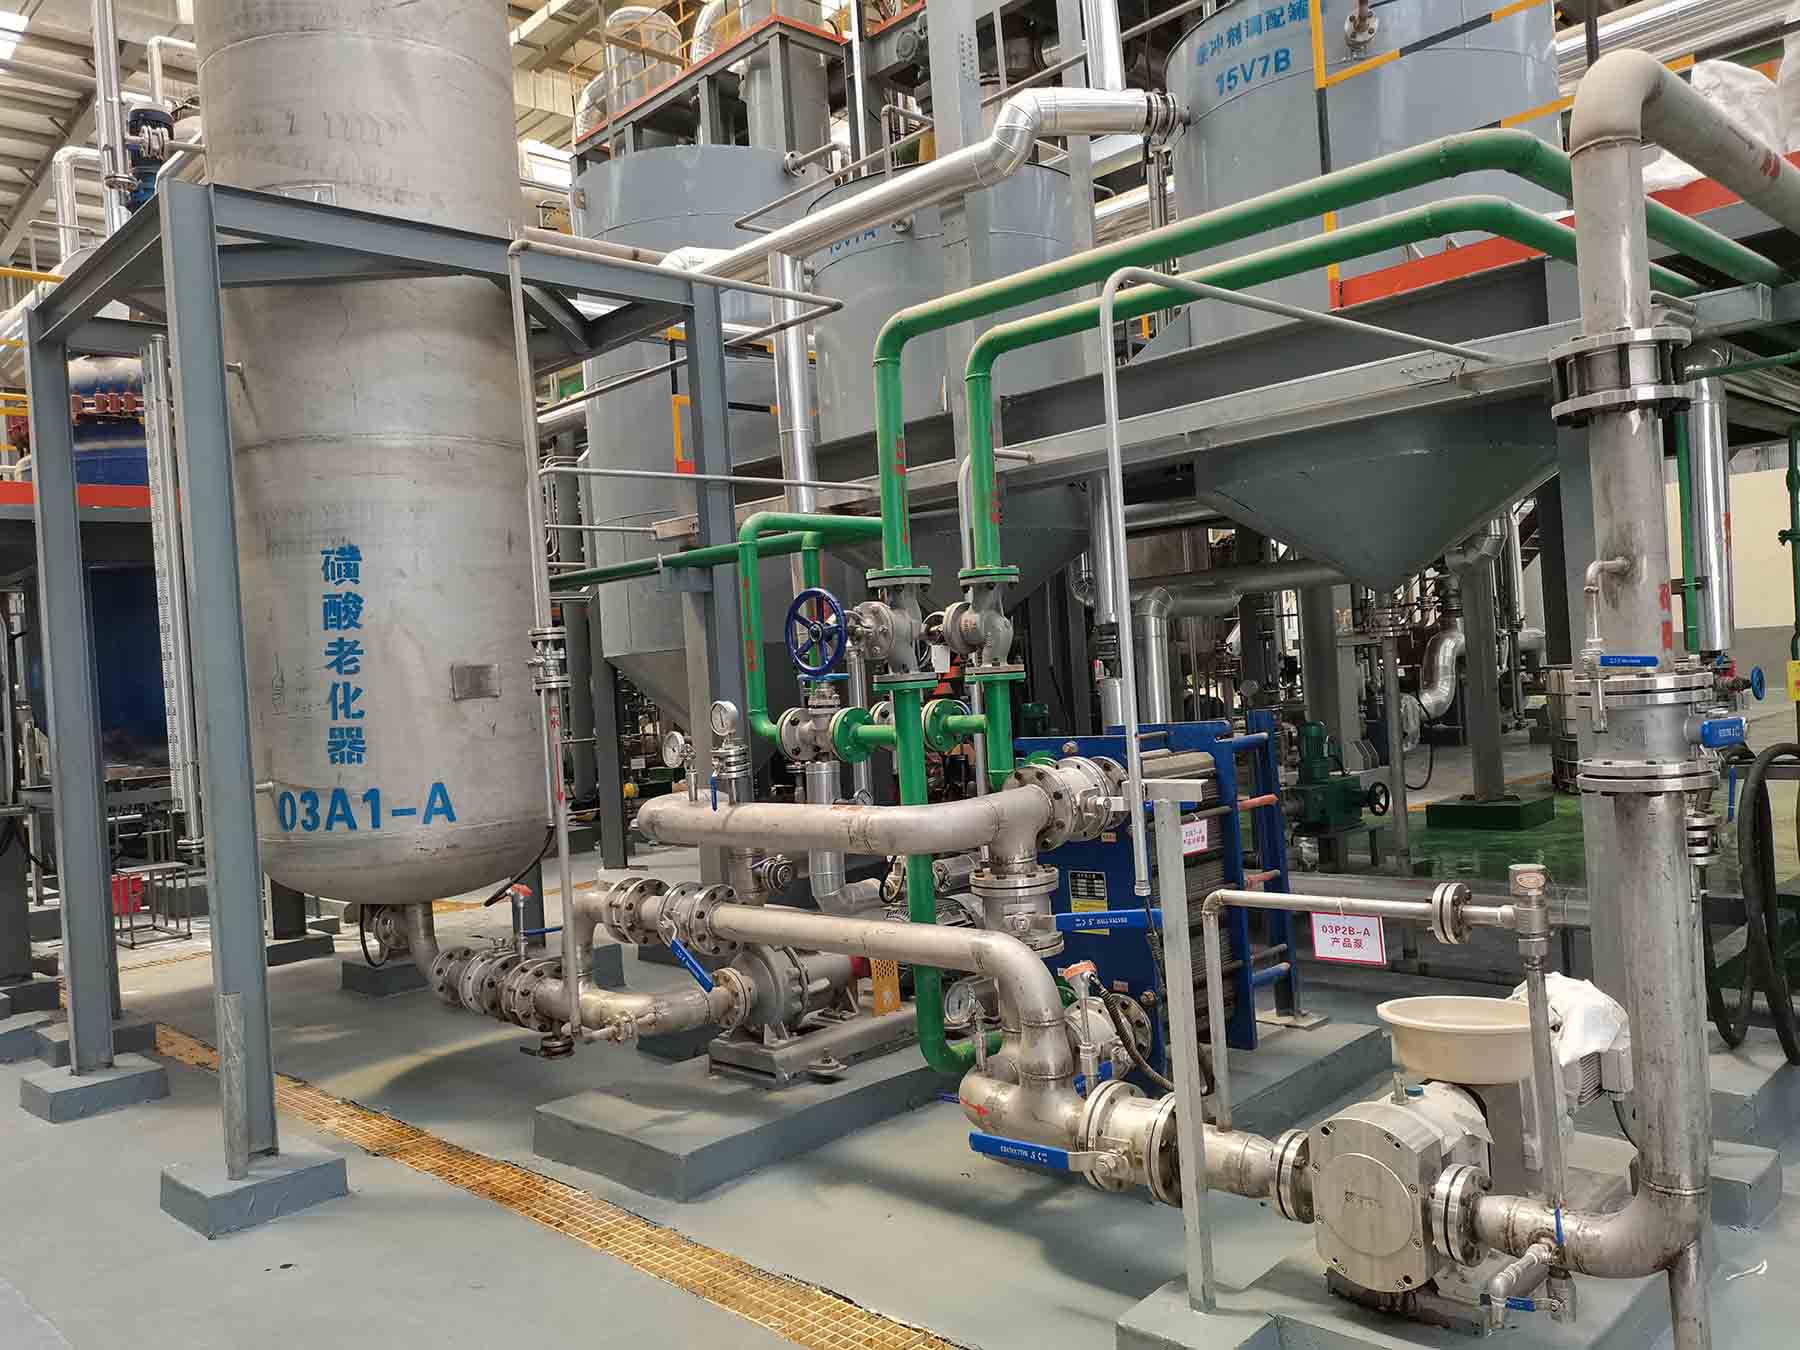
Unlike conventional agitated rotary aging vessels, our static unit provides a more homogeneous aging effect and eliminates back-mixing.
Equipped with proprietary internals, the static aging vessel ensures uniform residence time for all material molecules. In contrast, molecules in rotary aging vessels have non-uniform residence time following a normal distribution. The aging duration is adjustable from 0 to 60 minutes by regulating the liquid level inside the vessel. Typically, the aging time is set at 30 minutes. Where higher active matter content is required, e.g., for LABSA with active matter of 97.5%–98%, the aging time may be set to 45–60 minutes. In addition to superior process performance, this static equipment features lower power consumption and reduced maintenance demand.
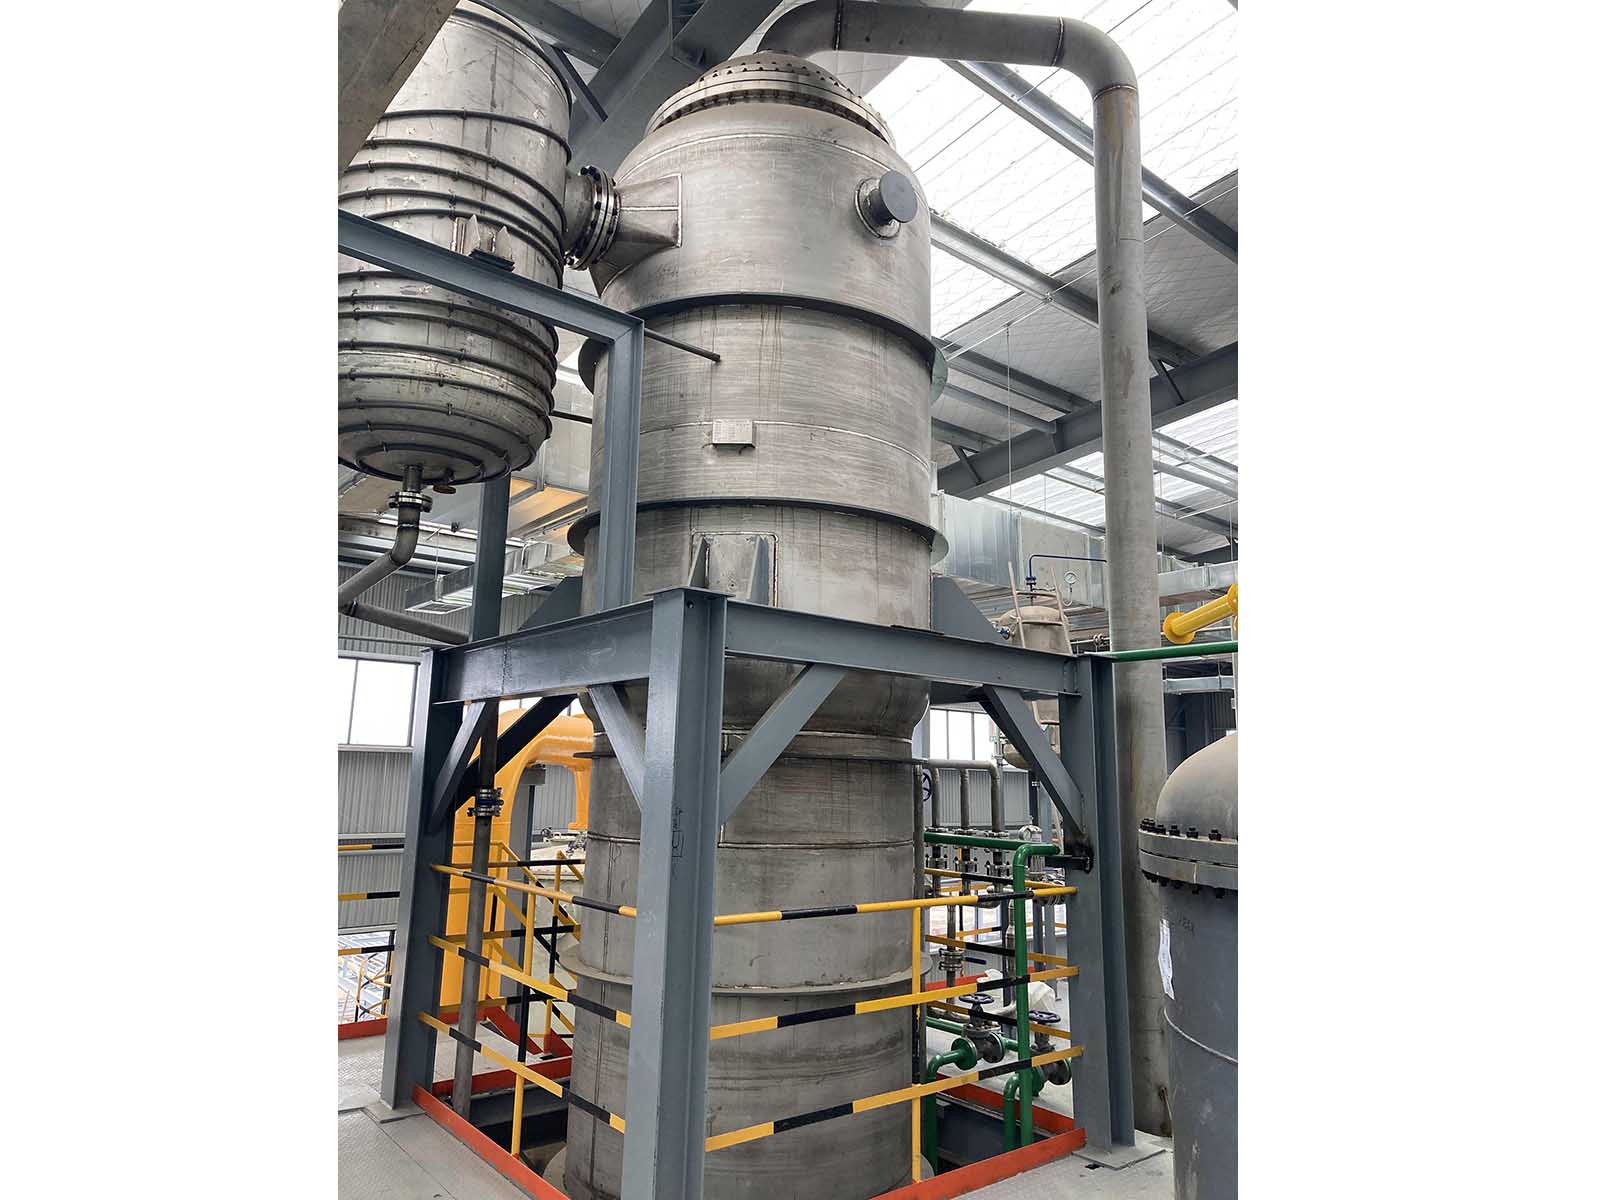
Stripping tower 79T1 is static equipment, without motor or rotating parts. Compared to outdated technology, our stripping tower doesn’t need maintenance. WEIXIAN designs the stripping tower based on the characteristic of sulfonated/sulphonated products. In the stripping tower, degassing, water removal, dioxane stripping, and cooling can be achieved in the same equipment, which can save power consumption, and ensure stable running and product quality.
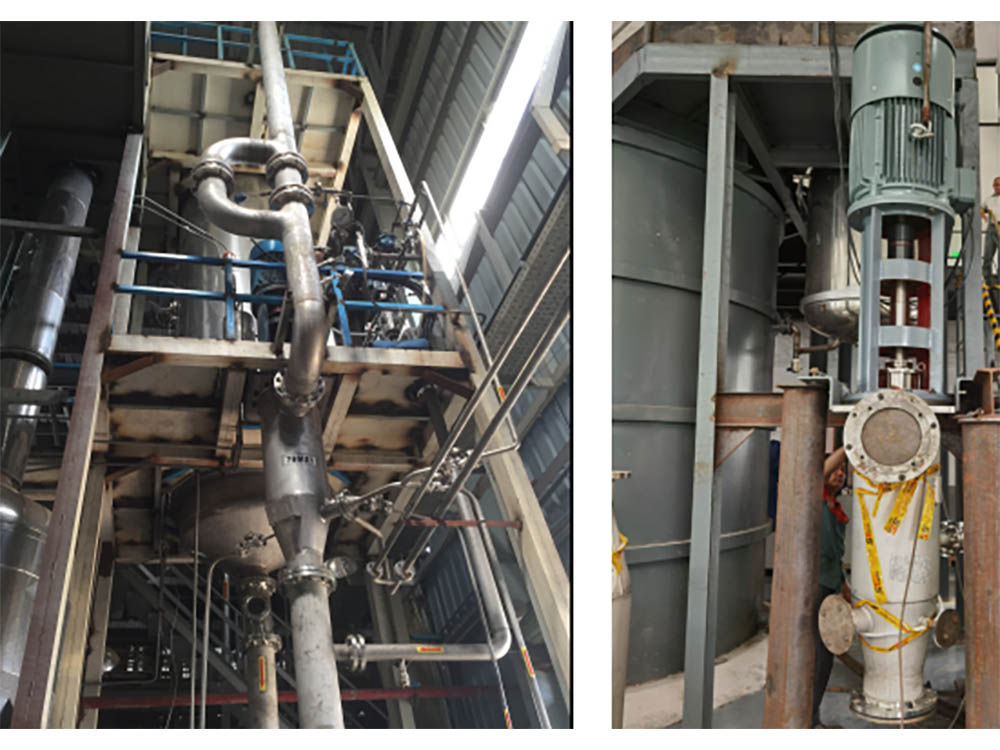
The high-shear neutralization reactor consists of multiple high-speed dispersing-shearing discs. Its mechanical seals and bearings are custom-designed for high-speed mixing and shearing service, enabling stable operation at 960 rpm.
This neutralization reactor features efficient and homogeneous mixing, flexible operation, stable system pressure and low failure rate.
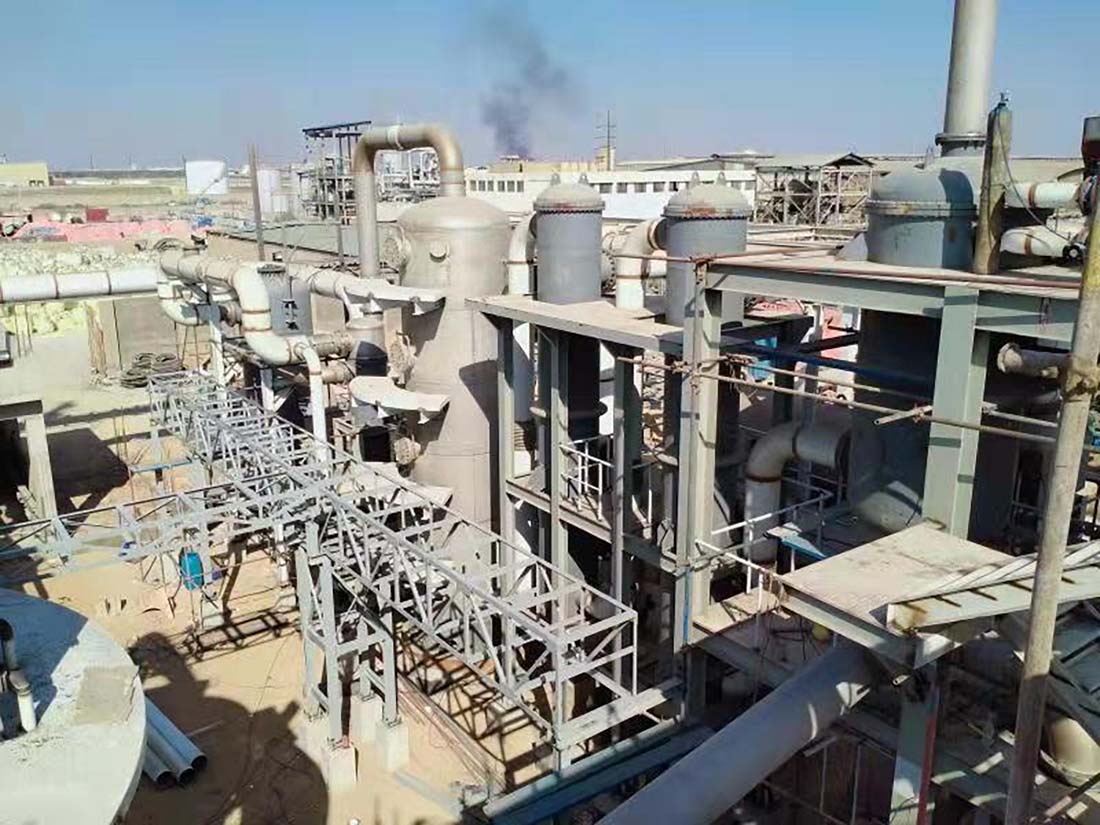
The converter adopts a vertical SS304 stainless steel packed tower structure with a maximum temperature resistance of 700°C.
It delivers stable conversion efficiency, flexible operational adjustment and precise temperature control, and achieves maintenance-free operation. The tower is configured with four packing layers filled with V₂O₅ composite catalysts combining low-temperature and medium-temperature catalytic formulations. This design not only realizes a low light-off temperature but also ensures an SO₂ conversion rate of over 98%. It significantly improves start-up preheating efficiency and reduces preheating duration.
Dedicated thermometer interfaces are reserved at the top and bottom of each catalyst bed to support accurate temperature regulation and sustain high conversion efficiency. Each bed is equipped with a manhole to facilitate on-site catalyst loading and replacement.
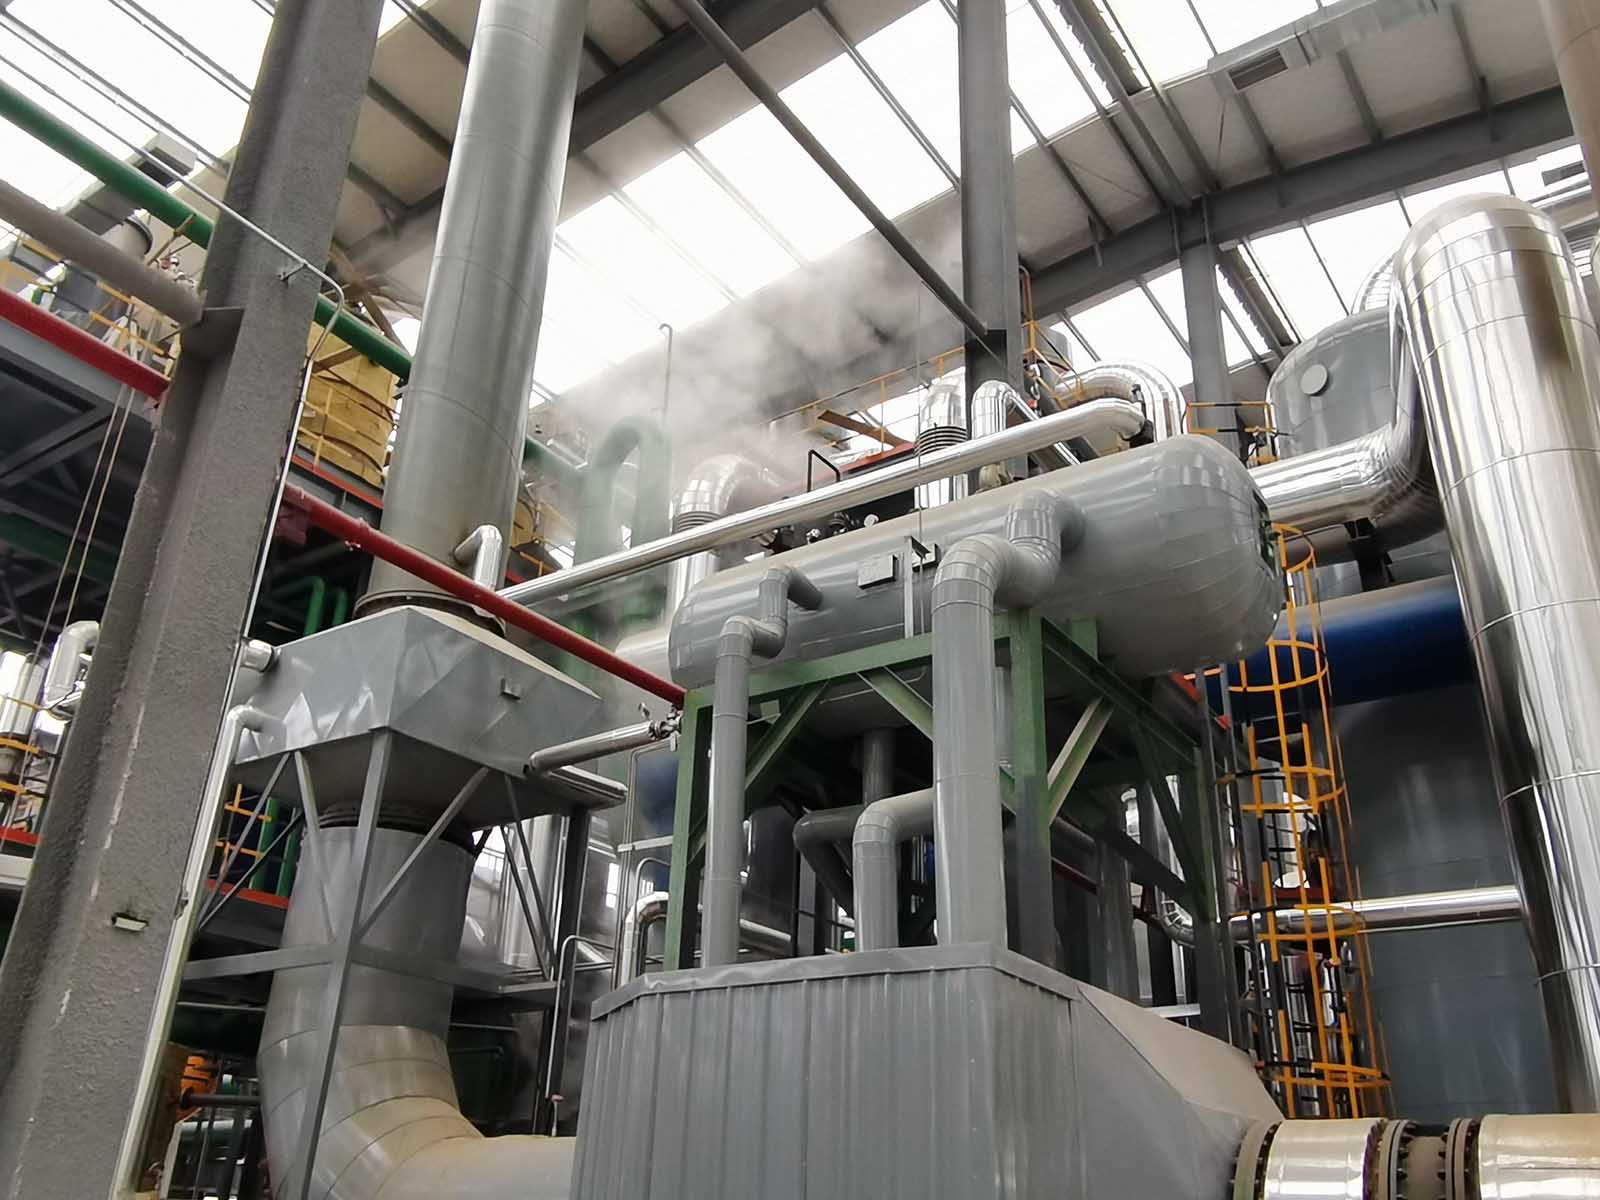
The heat-pipe heat exchanger features high heat transfer efficiency, compact structural layout and low flue-side flow resistance. With inherently safe and reliable structural characteristics, it outperforms conventional heat exchangers of other types. Damage to individual or a small number of heat pipes will not impair overall equipment performance or interrupt plant production. Since the water circuit is arranged externally to the flue gas duct, component replacement and routine overhaul can be performed without plant shutdown.
The equipment offers a design service life of over 10 years. Matched with the start-up preheater, the system can generate steam during cold start-up, eliminating the need for external steam supply.
Waste heat recovery performance is quantified as follows: 250 kg of steam is generated per 100 kg of sulfur combustion. The primary and secondary flue gas waste heat recovery stages produce steam, while the tertiary stage yields hot water, with corresponding heat recovery efficiencies of 36.5%, 44.2% and 67.3% respectively.
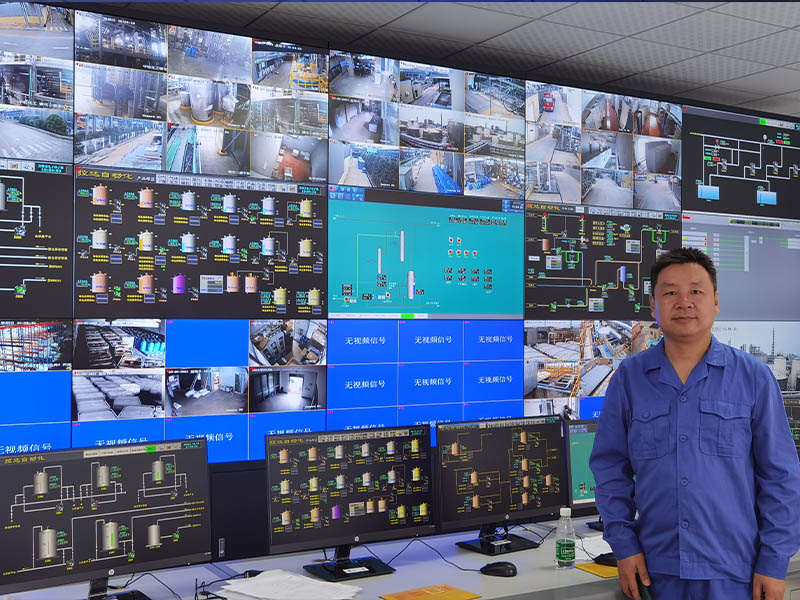
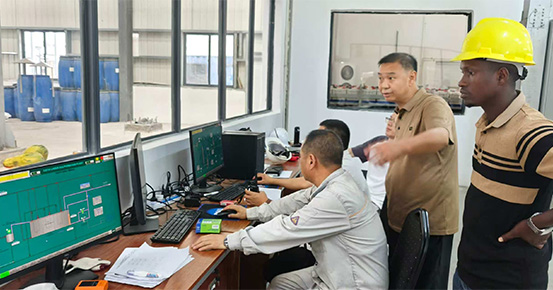
The control system adopts mainstream industrial brands including Siemens, ABB, Supcon, Hollysys, Honeywell or equivalent alternatives.
Field instruments are supplied by internationally renowned manufacturers: Emerson for mass flow meters, Michell for dew point meters, Mettler Toledo for pH meters, and Yokogawa for transmitters. Major electrical components are sourced from world-class brands such as Siemens, Schneider and ABB.
The entire plant is designed for high-level fully automatic operation. All programming and system configuration are completed by our in-house technical team. Remote parameter adjustment is available with the client’s authorization.
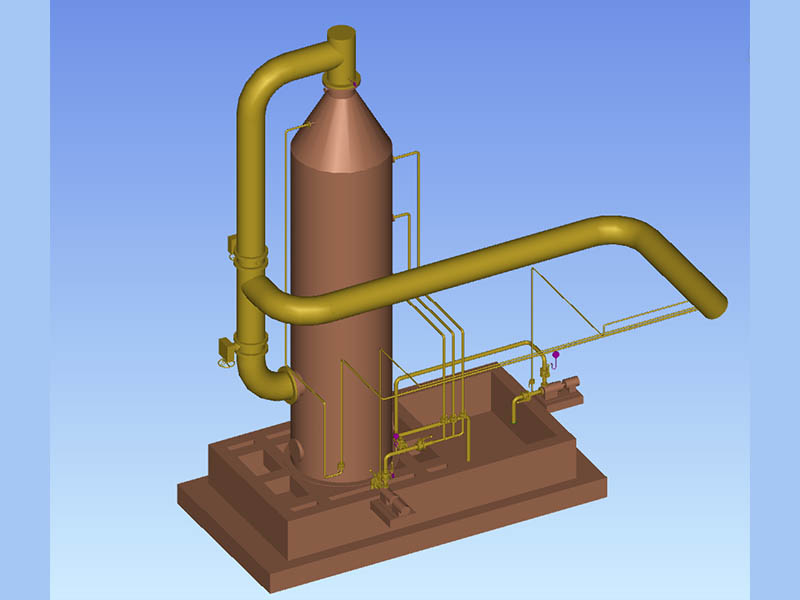
The hot air from the first bed of the converter and the SO₃ secondary cooler is used for silica gel regeneration; the excess hot air generates steam and hot water for heat tracing of raw materials and finished products. A portion of the remaining hot air (100 °C) is further sent to Unit 38 to treat the wastewater from the scrubber. By oxidizing the Na₂SO₃ and Na₂SO₄ in the wastewater and evaporating the water, crystalline Na₂SO₄ hydrate is produced. The plant can therefore achieve zero wastewater discharge from the scrubber.
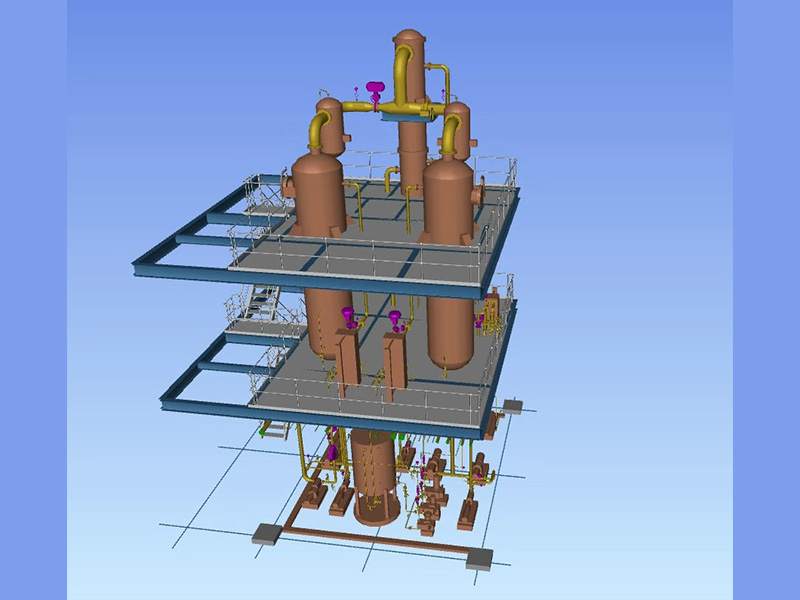
In recent years, WEIXIAN has focused intensively on ultra-low-dioxane technology. Building on the earlier Unit 79 Neutralization and Dioxane Stripping process, WEIXIAN has developed the new Unit 89 Dioxane Multi-stage Stripping process, which achieves a dioxane removal rate of 65%–99% as required. With this technology, a dioxane content below 1 ppm can be reliably achieved, regardless of the feedstock EO number or initial dioxane level.
In April 2026, WEIXIAN engineers successfully commissioned an ultra-low-dioxane system in South Korea.
Through careful optimization of operating parameters, the system achieved an 88.7% removal efficiency, reducing the dioxane concentration from 9.88 ppm to 1.13 ppm. The customer was highly satisfied with the results, and further reduction is available on request.
This breakthrough enables any sulphation plant to meet the strictest SLES dioxane limits required by high-end markets, while keeping costs relatively low.
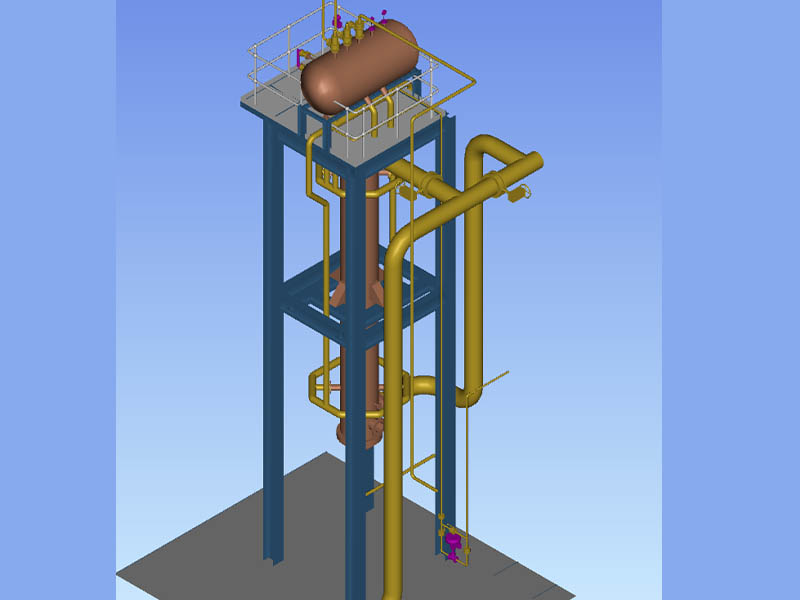
The reaction heat released from the sulfur combustion furnace and SO₂/SO₃ converter is recovered and directly converted into steam via a fire-tube boiler.
Compared with conventional processes, this advanced heat recovery system doubles steam production capacity. The generated steam not only satisfies the steam demand of the sulfur melting unit, but also completely meets the cooling requirement of the air drying unit. By adopting a steam-driven lithium bromide chiller to replace the conventional electric chiller for chilled water production, the overall system power consumption is reduced by 15%.
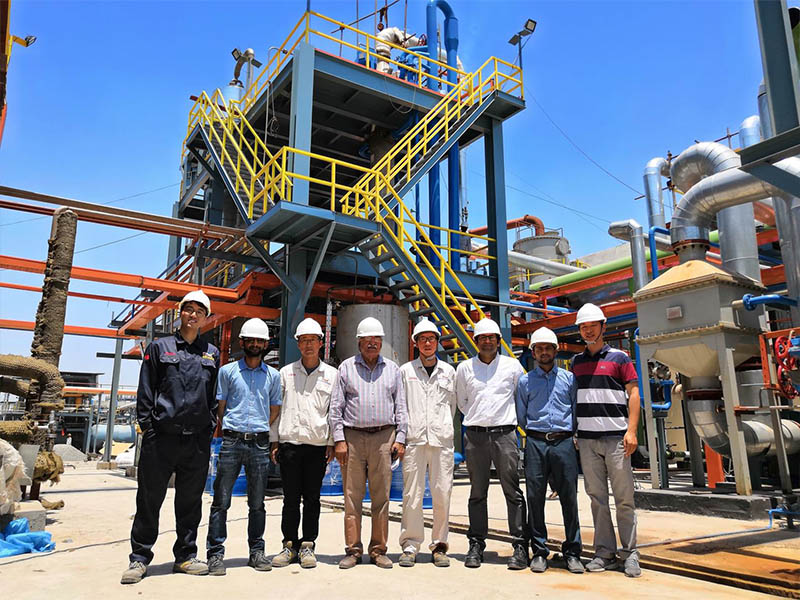
Apart from advanced core process technology, we prioritize comprehensive after-sales technical services and professional training for clients. We provide a 10-hour global response service for customer inquiries and technical issues, and our professional technicians can be dispatched to any worldwide location within 72 hours.
Benefiting from the high stability and reliability of our process design, WEIXIAN sulfonation plants achieve an annual operating rate of 330 days. A full one-year warranty is provided for all complete sets of equipment. Meanwhile, we recommend clients to equip with our standard spare parts kits for timely replacement of wearing parts, which are supplied at cost price.
WEIXIAN provides a full range of professional technical services covering:
1. Free ongoing technical consultation.
2. Pre-project feasibility study analysis.
3. Quotation and technical proposal for integrated turnkey sulfonation plants and individual equipment.
4. Upgrading, renovation and technical revamp of existing sulfonation production lines.
5. Customized design and engineering of turnkey sulfonation plants and supporting equipment.
6. On-site plant installation and assembly service.
7. Remote and on-site technical support as well as complete plant commissioning.
8. Professional operational and maintenance training for client technical personnel.
9. All other technical services related to sulfonation process production.
OVER 30 YEARS HISTORY
CARRIED OUT OVER 200 PROJECTS
Supplied The World Largest 8T/H Plant
COVERED 17 COUNTRIES IN THE WORLD


Building 20, Baijiahui Innovation Community 2, 699-18 Xuanwu Avenue, Nanjing, China
© 2026 WEIXIAN (Nanjing) Science Technology co., ltd. All Rights Reserved.