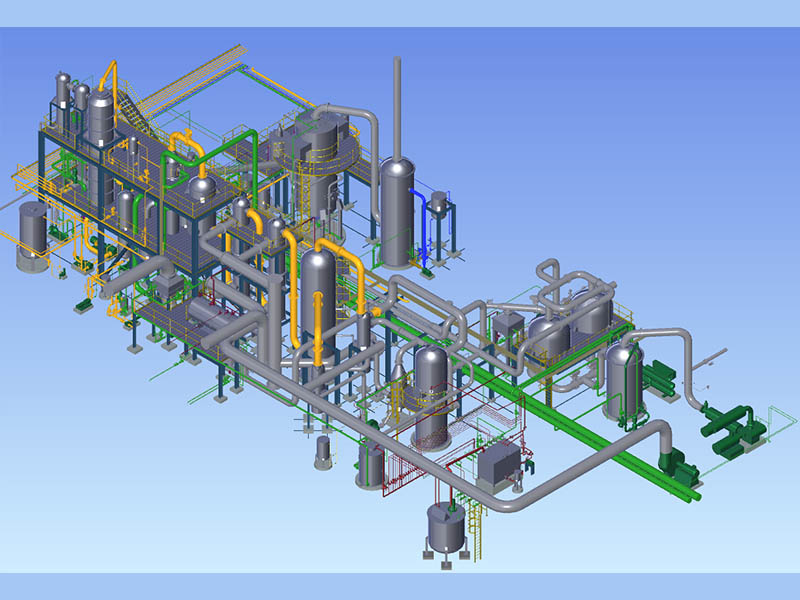
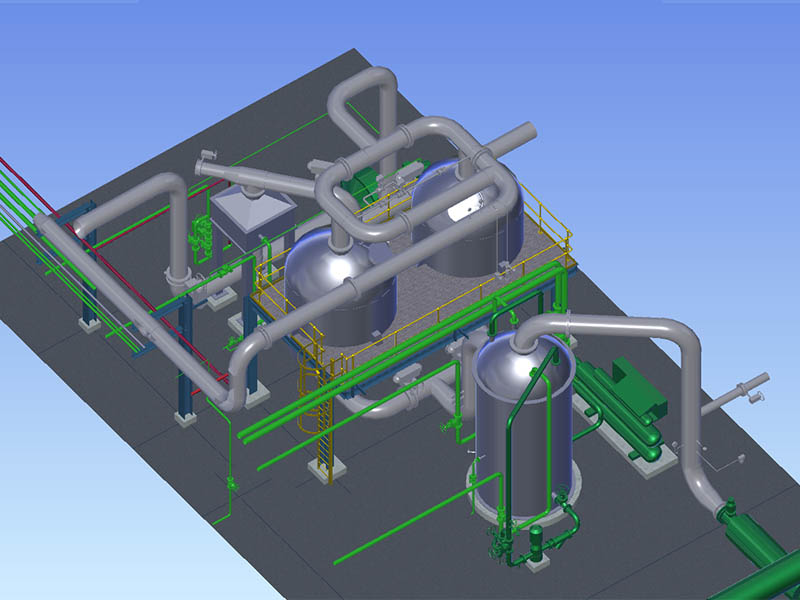
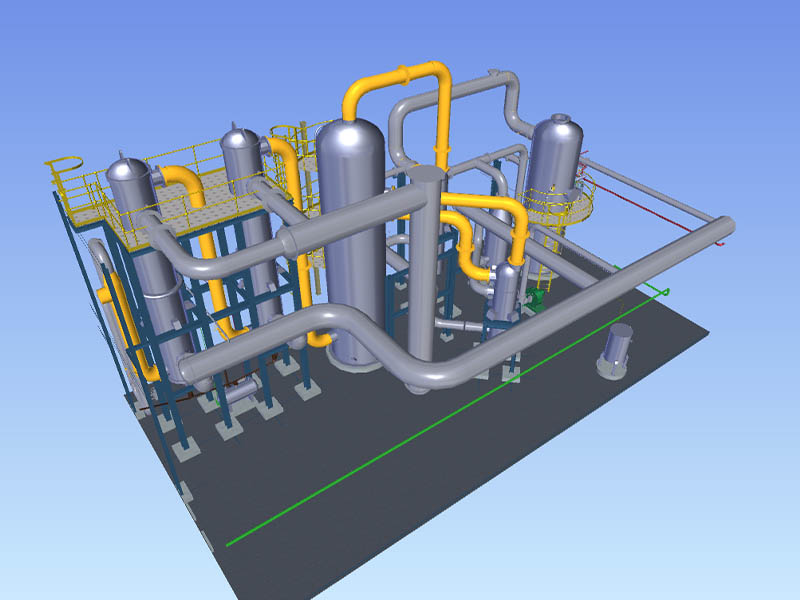
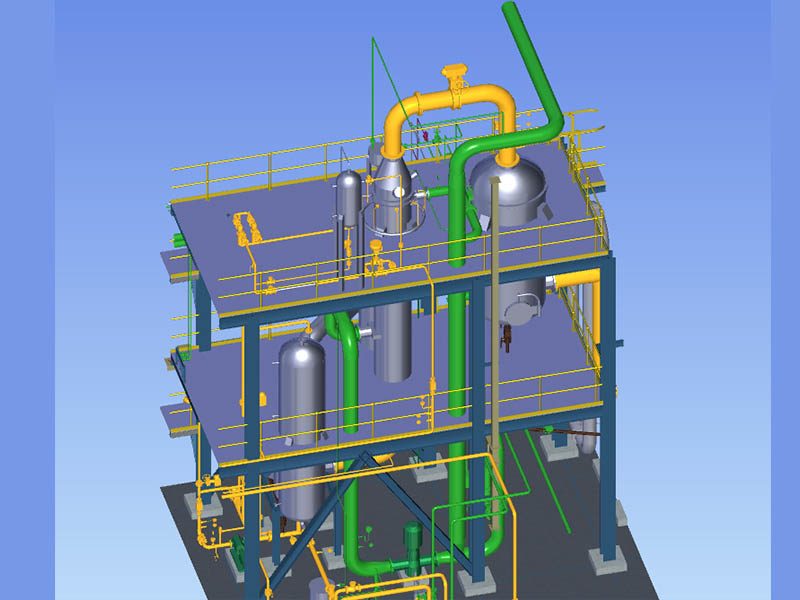
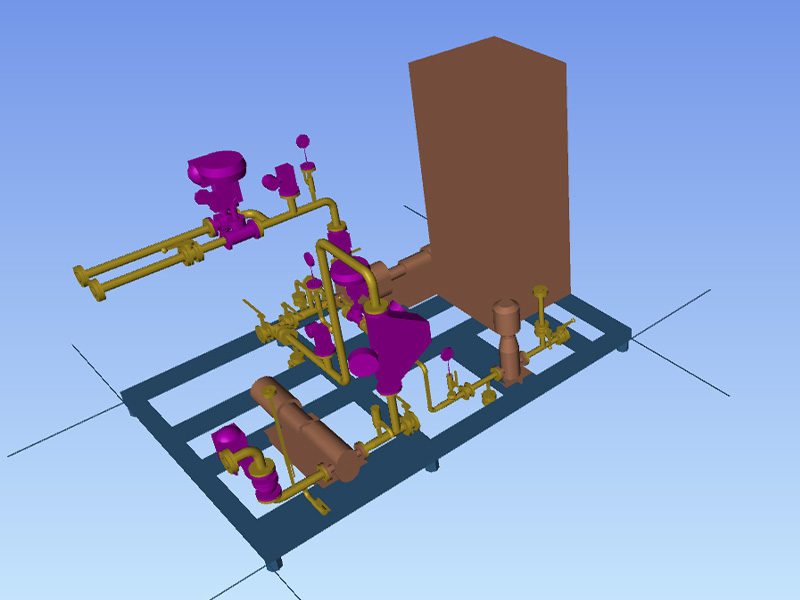
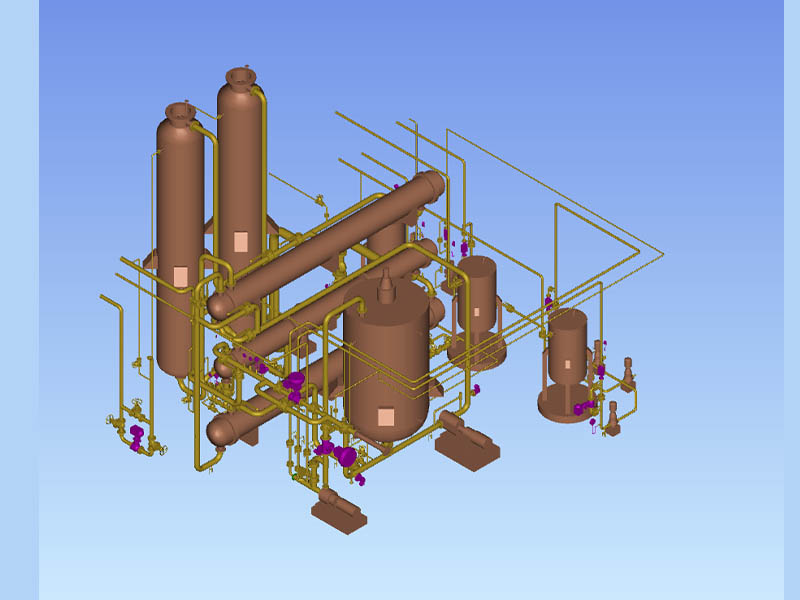
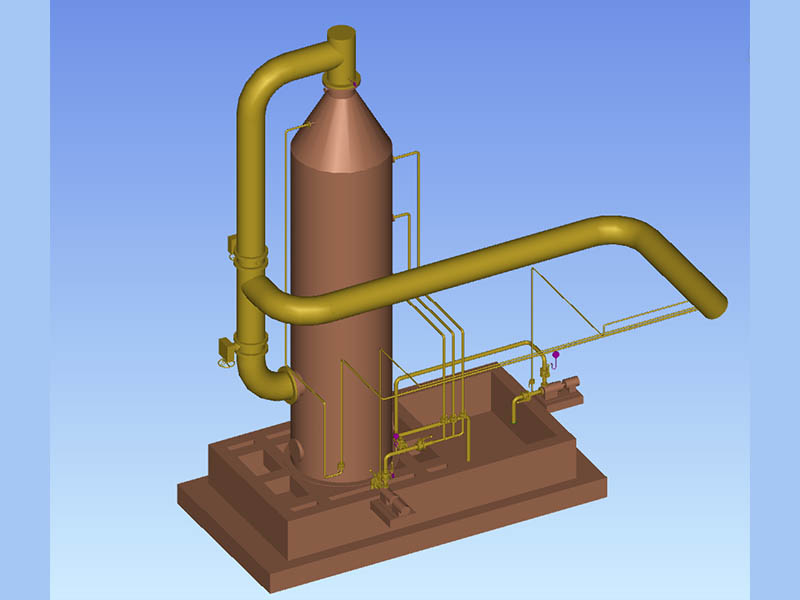
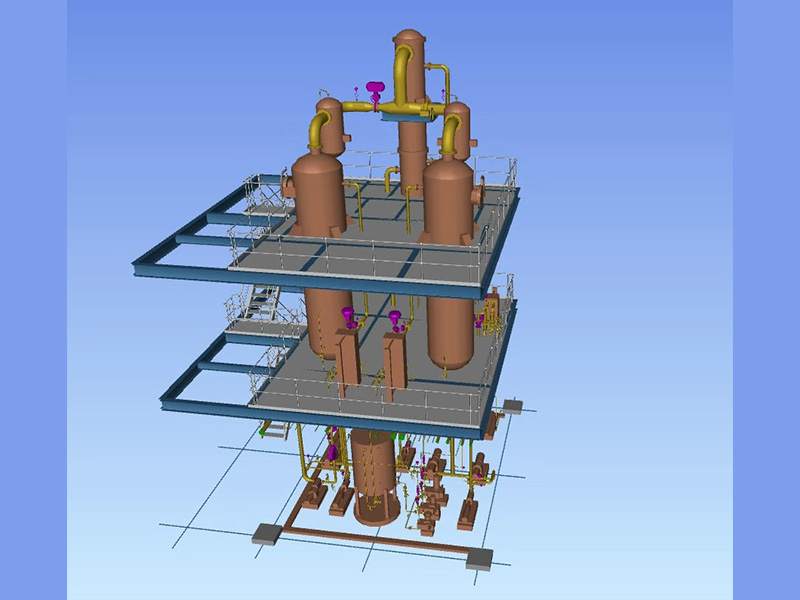
WEIXIAN sulphonation/sulfonation plants represent the highest level in the industry. So far, we can provide from a one-tube pilot plant to 10t/h mass production plant. Among 200+ projects we have done, the majority of them were turnkey basis, including but not limited to:
· LABSA (sulfonic acid) production line · SLES production line · SLS production line · AOS production line · HABSA production line · MES production line · SLS/AOS/sulfonic acid sodium salt drying units · Other anionic surfactant production lines
By adopting state-of-the-art designs and processes, all the performance aspects including plant reliability, finished product qualities, and unit raw material/power consumption are superior to that of competitive plants.
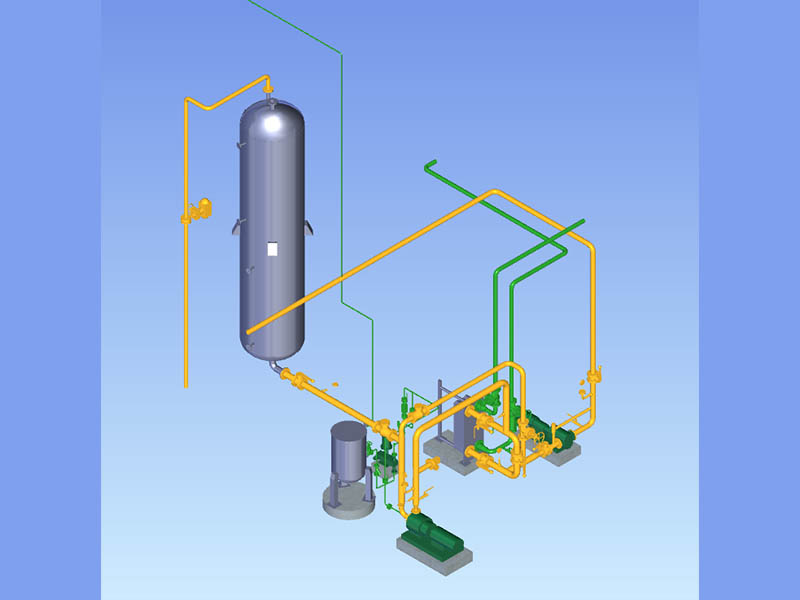
Liquid or solid sulfur is fed into pipelines insulated with steam coils and jackets, then delivered to the sulfur melting tank. The molten sulfur is subsequently pumped to the high-level tank and further conveyed to the sulfur burner by a submerged gear pump or a gear pump with steam-jacket insulation. By integrating a mass flow meter with a variable-frequency drive (VFD) on the gear pump, the flow rate of liquid sulfur is maintained at a stable and controlled rate.
Features: The WEIXIAN liquid sulfur gear pump resists clogging by impurities. With the flow rate regulated by a mass flow meter and VFD, delivery is stable and accurate. The system also enables online monitoring of operating parameters, offering maximum convenience for controlling SO₃ concentration, adjusting plant performance, and switching product grades.
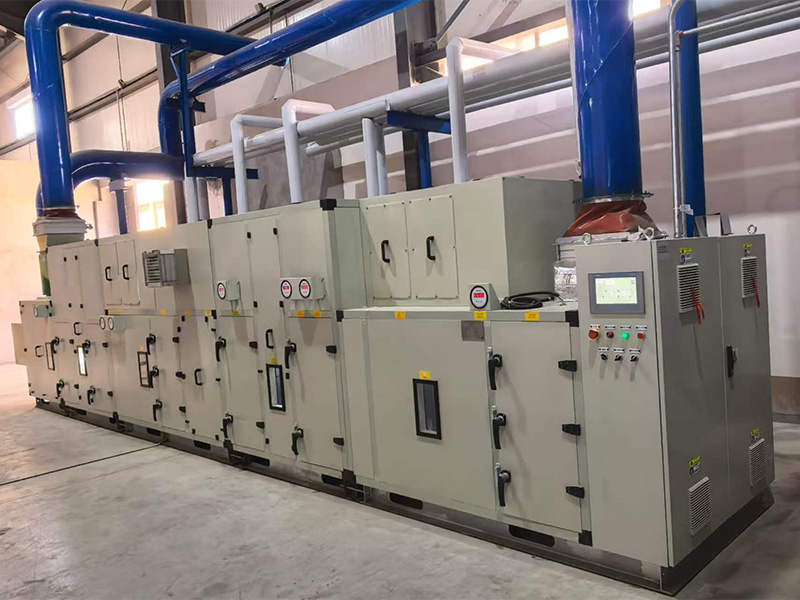
The Problem with Conventional Drying: Traditional dual tank drying systems cycle between adsorption and regeneration every eight hours – causing flow and temperature swings, dew point drift, valve wear, and constant operator attention.
WEIXIAN's Answer: Unit 22. A single, continuously rotating silica gel bed that eliminates switching entirely. A World First from WEIXIAN.
Key Advantages
8,000 hours/year continuous operation – no 8 hour tank switching
Stable air flow and temperature – no switching transients
Constant dew point at –65 °C ± 3 °C
Better, more consistent product quality
20+kWh lower plant overall power consumption
Simpler, more convenient operation
Atmospheric air is compressed by the main blower and fed to a dehumidifier, where most of the moisture is removed by water cooling and refrigeration. The air then passes through a silica gel bed for deep dehumidification, ultimately producing dry air with a dew point of −60 °C. The flow rate of dry air (Nm³/h or kg/h) is regulated by the speed of the main blower, which is controlled in closed loop by an orifice flow meter and the blower's variable-frequency drive (VFD).
Features: The air-cooling finned heat exchanger uses SS304 stainless steel for both fins and tubes, delivering a service life far longer than that of conventional copper-tube/aluminum-fin construction.
Liquid sulfur is precisely metered and fed to the sulfur burner, where it fully combusts with dry air to generate SO₂. After cooling, the SO₂ gas enters the converter and is converted to SO₃ over a vanadium catalyst. Following further cooling, the SO₃ gas is sent to the sulphonation/sulfation unit. The SO₂ and SO₃ gases are cooled by cooling air in a tube-type heat exchanger; the resulting hot air is collected and routed to the waste heat recovery unit to generate steam and hot water. The secondary hot air is then used for silica gel regeneration and for the evaporation and crystallization of scrubber wastewater in Unit 38.
Features: The SO₂ cooler adopts inlet-end insulation protection and a floating-tube design, which prevents intergranular corrosion of the stainless steel above 600 °C and doubles the service life. By integrating the start-up pre-heater with the waste heat recovery unit, the steam produced during converter preheating is also used for sulfur melting and hot-water generation, so that WEIXIAN plants require no external steam.
SO₃ gas, adjusted to a precise concentration (%), passes through an SO₃ filter and then reacts with the organic raw material in the reactor. The heat of reaction is removed by circulating cooling water on the shell side of the reactor. The exhaust gas passes through a gas–liquid separator and a cyclone separator before entering the exhaust-gas treatment unit, while the organic acid is sent to an aging and stabilization unit, or to a neutralization and dioxane-stripping unit.
The flow rate of the organic raw material is controlled by a mass flow meter and a control valve (or by the VFD of a gear pump). The liquid level in the gas–liquid separator is controlled by a level transmitter and the VFD of the discharge pump. The flow rate and density of the organic acid are measured by a mass flow meter, with density under cascade control to trim the raw-material flow rate. The inlet temperature of the circulating cooling water is held constant by makeup water, and the cooling-water flow is regulated by a control valve whose opening depends on the reactor temperature difference on each pass.
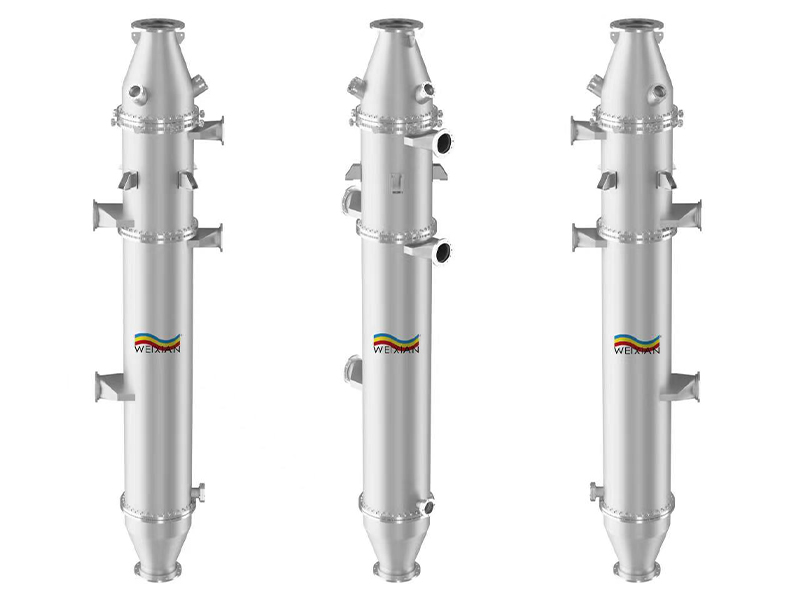
Features: WEIXIAN incorporates more than three key design improvements to enhance reactor reliability. The dimensions of every reactor tube, distributor and nozzle are manufactured to a high degree of uniformity. Each reactor tube is produced by high-precision rolling followed by an oxygen-free annealing process, so that the surface finish is uniform across all tubes and along the length of each tube. Compared with competing technologies, WEIXIAN plants deliver longer continuous operating runs and lower dioxane levels when producing SLES.
The LABSA (linear alkylbenzene sulphonic acid) from the separator is fed to the aging vessel by the first discharge pump, then stabilized with water in the stabilization pump. After cooling, the LABSA is pumped to the finished-product tanks by the second discharge pump. The liquid level in the aging vessel is controlled by a level transmitter and the VFD of the second discharge pump.
Features: The WEIXIAN aging vessel is of vertical, static-mixing construction with no back-mixing, and the aging time is precisely controlled. This brings the aging conversion rate close to its theoretical limit, minimizes the free-oil and free-sulfuric-acid content, and correspondingly raises the active-matter content to or toward 98%.
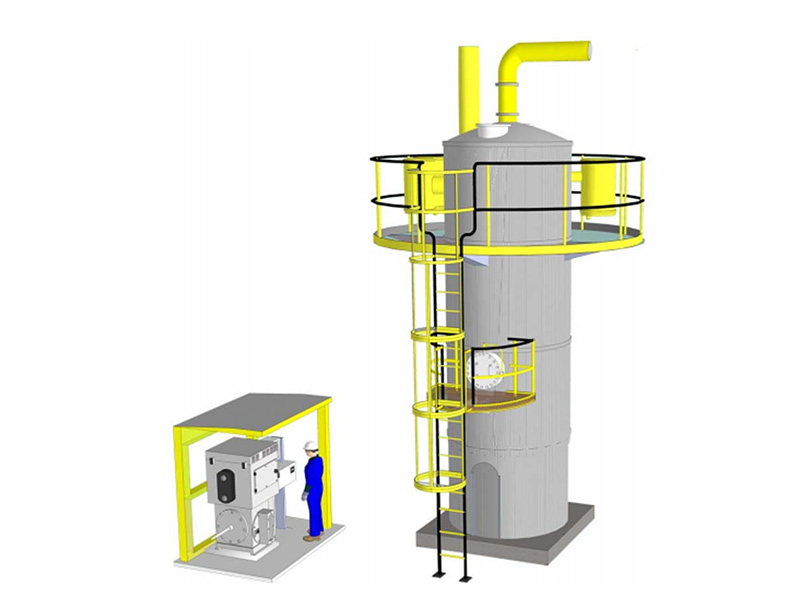
Before discharge, the exhaust gas is treated to remove organic acid mist and SO₃ in an electrostatic precipitator (ESP), while SO₂ is removed in a scrubber.
Features: WEIXIAN uses plate-type tubes as the ESP cathode. Compared with steel-wire cathodes, this design requires no maintenance.
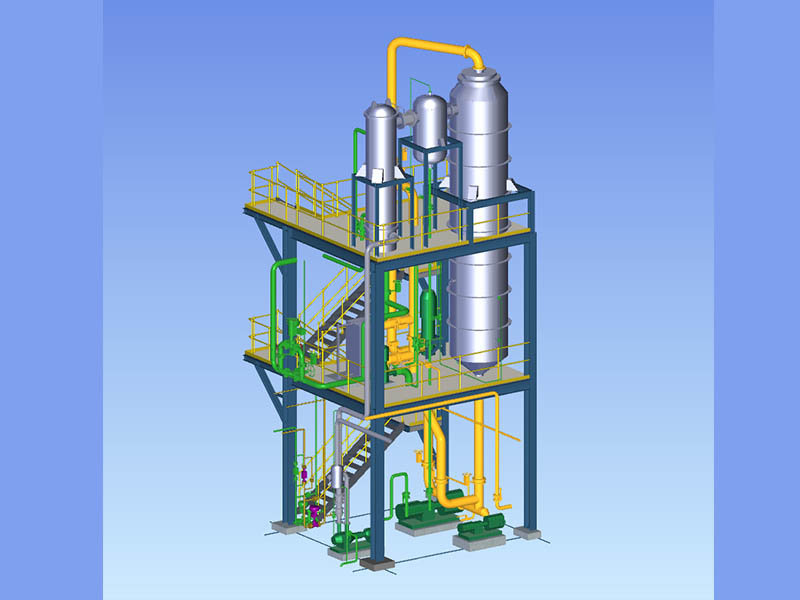
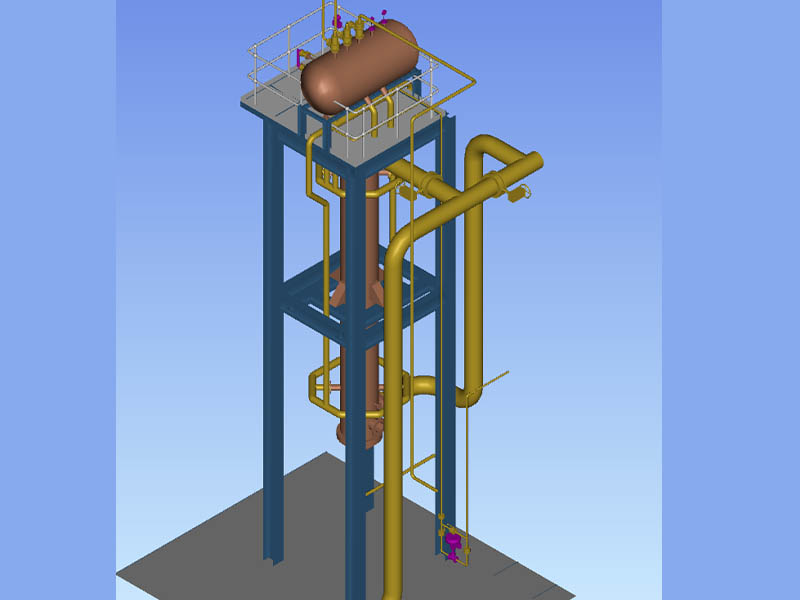
When producing SLES, the sulfate is neutralized with pure water, caustic soda, hydrogen peroxide (H₂O₂) and a buffer in the neutralization reactor, where all ingredients are brought to reaction by high-shear mixing. Dioxane is then stripped out together with air in the stripping tower under vacuum, while cooling is also carried out in the same tower.
Features: Compared with other vacuum-neutralization process, the WEIXIAN stripping tower is a static unit with no motor and requires no maintenance. The product is reacted in a micro-positive-pressure reactor before entering the stripping tower, so that no acid-gas corrosion occurs in the condensate or the vacuum pump. The unit also incorporates a ten-times SLES recycle loop. Compared with similar technologies from other suppliers, this process keeps the neutralization temperature rise below 5 °C, yielding products with a lighter color, a more stable pH and lower dioxane content. The unit can achieve ultra-low dioxane levels.
The hot air first enters the heat-pipe exchanger, where heat is transferred to the soft water inside, generating steam at 0.4–0.6 MPa. After leaving the heat-pipe exchanger, the hot air is further used to pre-heat the reverse-osmosis (R/O) water and produce hot water.
Features: With the waste heat recovery system, the plant requires no external steam for cold start-up. During normal operation, the plant achieves full steam and hot-water self-sufficiency.
The dilution system is purpose-built for the online dilution of high-concentration (70%) SLES/SLS down to 25%–30%. It is available in two capacity ranges: 2–8 t/h and 4–10 t/h.
Its key advantage is that the SLES/SLS production units no longer need to be cleaned when switching between product concentrations. The high-concentration product can be produced and stored in tanks for extended periods; whenever a low-concentration product is required, the system dilutes it on demand, at any time. This greatly improves production and sales flexibility and convenience.
In addition, the system can be supplied as a skid-mounted unit: only the finished-product tank piping needs to be connected before commissioning. The complete package includes all online production equipment, a control panel and the control system.
The sulfolactone hydrolysis system consists of a boosting pump, three heat exchangers and a hydrolyzer. After aging, the α-olefin sulfonate is fed, together with pure water, caustic soda, hydrogen peroxide solution and buffer, into the neutralization reactor. Following high-shear mixing, the mixture is pumped through two heat exchangers and the hydrolyzer in sequence; after hydrolysis, the finished product AOS is obtained.
WEIXIAN sulphonation/sulfonation plants represent the highest level in the industry. So far, we can provide from a one-tube pilot plant to 10t/h mass production plant. Among 200+ projects we have done, the majority of them were turnkey basis, including but not limited to:
· LABSA (sulfonic acid) production line · SLES production line · SLS production line · AOS production line · HABSA production line · MES production line · SLS/AOS/sulfonic acid sodium salt drying units · Other anionic surfactant production lines
By adopting state-of-the-art designs and processes, all the performance aspects including plant reliability, finished product qualities, and unit raw material/power consumption are superior to that of competitive plants.
Liquid or solid sulfur is fed into pipelines insulated with steam coils and jackets, then delivered to the sulfur melting tank. The molten sulfur is subsequently pumped to the high-level tank and further conveyed to the sulfur burner by a submerged gear pump or a gear pump with steam-jacket insulation. By integrating a mass flow meter with a variable-frequency drive (VFD) on the gear pump, the flow rate of liquid sulfur is maintained at a stable and controlled rate.
Features: The WEIXIAN liquid sulfur gear pump resists clogging by impurities. With the flow rate regulated by a mass flow meter and VFD, delivery is stable and accurate. The system also enables online monitoring of operating parameters, offering maximum convenience for controlling SO₃ concentration, adjusting plant performance, and switching product grades.
The Problem with Conventional Drying: Traditional dual tank drying systems cycle between adsorption and regeneration every eight hours – causing flow and temperature swings, dew point drift, valve wear, and constant operator attention.
WEIXIAN's Answer: Unit 22. A single, continuously rotating silica gel bed that eliminates switching entirely. A World First from WEIXIAN.
Key Advantages
8,000 hours/year continuous operation – no 8 hour tank switching
Stable air flow and temperature – no switching transients
Constant dew point at –65 °C ± 3 °C
Better, more consistent product quality
20+kWh lower plant overall power consumption
Simpler, more convenient operation
Atmospheric air is compressed by the main blower and fed to a dehumidifier, where most of the moisture is removed by water cooling and refrigeration. The air then passes through a silica gel bed for deep dehumidification, ultimately producing dry air with a dew point of −60 °C. The flow rate of dry air (Nm³/h or kg/h) is regulated by the speed of the main blower, which is controlled in closed loop by an orifice flow meter and the blower's variable-frequency drive (VFD).
Features: The air-cooling finned heat exchanger uses SS304 stainless steel for both fins and tubes, delivering a service life far longer than that of conventional copper-tube/aluminum-fin construction.
Liquid sulfur is precisely metered and fed to the sulfur burner, where it fully combusts with dry air to generate SO₂. After cooling, the SO₂ gas enters the converter and is converted to SO₃ over a vanadium catalyst. Following further cooling, the SO₃ gas is sent to the sulphonation/sulfation unit. The SO₂ and SO₃ gases are cooled by cooling air in a tube-type heat exchanger; the resulting hot air is collected and routed to the waste heat recovery unit to generate steam and hot water. The secondary hot air is then used for silica gel regeneration and for the evaporation and crystallization of scrubber wastewater in Unit 38.
Features: The SO₂ cooler adopts inlet-end insulation protection and a floating-tube design, which prevents intergranular corrosion of the stainless steel above 600 °C and doubles the service life. By integrating the start-up pre-heater with the waste heat recovery unit, the steam produced during converter preheating is also used for sulfur melting and hot-water generation, so that WEIXIAN plants require no external steam.
SO₃ gas, adjusted to a precise concentration (%), passes through an SO₃ filter and then reacts with the organic raw material in the reactor. The heat of reaction is removed by circulating cooling water on the shell side of the reactor. The exhaust gas passes through a gas–liquid separator and a cyclone separator before entering the exhaust-gas treatment unit, while the organic acid is sent to an aging and stabilization unit, or to a neutralization and dioxane-stripping unit.
The flow rate of the organic raw material is controlled by a mass flow meter and a control valve (or by the VFD of a gear pump). The liquid level in the gas–liquid separator is controlled by a level transmitter and the VFD of the discharge pump. The flow rate and density of the organic acid are measured by a mass flow meter, with density under cascade control to trim the raw-material flow rate. The inlet temperature of the circulating cooling water is held constant by makeup water, and the cooling-water flow is regulated by a control valve whose opening depends on the reactor temperature difference on each pass.
Features: WEIXIAN incorporates more than three key design improvements to enhance reactor reliability. The dimensions of every reactor tube, distributor and nozzle are manufactured to a high degree of uniformity. Each reactor tube is produced by high-precision rolling followed by an oxygen-free annealing process, so that the surface finish is uniform across all tubes and along the length of each tube. Compared with competing technologies, WEIXIAN plants deliver longer continuous operating runs and lower dioxane levels when producing SLES.
The LABSA (linear alkylbenzene sulphonic acid) from the separator is fed to the aging vessel by the first discharge pump, then stabilized with water in the stabilization pump. After cooling, the LABSA is pumped to the finished-product tanks by the second discharge pump. The liquid level in the aging vessel is controlled by a level transmitter and the VFD of the second discharge pump.
Features: The WEIXIAN aging vessel is of vertical, static-mixing construction with no back-mixing, and the aging time is precisely controlled. This brings the aging conversion rate close to its theoretical limit, minimizes the free-oil and free-sulfuric-acid content, and correspondingly raises the active-matter content to or toward 98%.
Before discharge, the exhaust gas is treated to remove organic acid mist and SO₃ in an electrostatic precipitator (ESP), while SO₂ is removed in a scrubber.
Features: WEIXIAN uses plate-type tubes as the ESP cathode. Compared with steel-wire cathodes, this design requires no maintenance.
When producing SLES, the sulfate is neutralized with pure water, caustic soda, hydrogen peroxide (H₂O₂) and a buffer in the neutralization reactor, where all ingredients are brought to reaction by high-shear mixing. Dioxane is then stripped out together with air in the stripping tower under vacuum, while cooling is also carried out in the same tower.
Features: Compared with other vacuum-neutralization process, the WEIXIAN stripping tower is a static unit with no motor and requires no maintenance. The product is reacted in a micro-positive-pressure reactor before entering the stripping tower, so that no acid-gas corrosion occurs in the condensate or the vacuum pump. The unit also incorporates a ten-times SLES recycle loop. Compared with similar technologies from other suppliers, this process keeps the neutralization temperature rise below 5 °C, yielding products with a lighter color, a more stable pH and lower dioxane content. The unit can achieve ultra-low dioxane levels.
The hot air first enters the heat-pipe exchanger, where heat is transferred to the soft water inside, generating steam at 0.4–0.6 MPa. After leaving the heat-pipe exchanger, the hot air is further used to pre-heat the reverse-osmosis (R/O) water and produce hot water.
Features: With the waste heat recovery system, the plant requires no external steam for cold start-up. During normal operation, the plant achieves full steam and hot-water self-sufficiency.
The dilution system is purpose-built for the online dilution of high-concentration (70%) SLES/SLS down to 25%–30%. It is available in two capacity ranges: 2–8 t/h and 4–10 t/h.
Its key advantage is that the SLES/SLS production units no longer need to be cleaned when switching between product concentrations. The high-concentration product can be produced and stored in tanks for extended periods; whenever a low-concentration product is required, the system dilutes it on demand, at any time. This greatly improves production and sales flexibility and convenience.
In addition, the system can be supplied as a skid-mounted unit: only the finished-product tank piping needs to be connected before commissioning. The complete package includes all online production equipment, a control panel and the control system.
The sulfolactone hydrolysis system consists of a boosting pump, three heat exchangers and a hydrolyzer. After aging, the α-olefin sulfonate is fed, together with pure water, caustic soda, hydrogen peroxide solution and buffer, into the neutralization reactor. Following high-shear mixing, the mixture is pumped through two heat exchangers and the hydrolyzer in sequence; after hydrolysis, the finished product AOS is obtained.
WEIXIAN is an engineering company specialized in supplying turnkey sulphonation/sulphation plant and it's technology, focusing on the R&D of LABSA, SLES, SLS, AOS, HABSA, MES and other anionic surfactant production technologies.