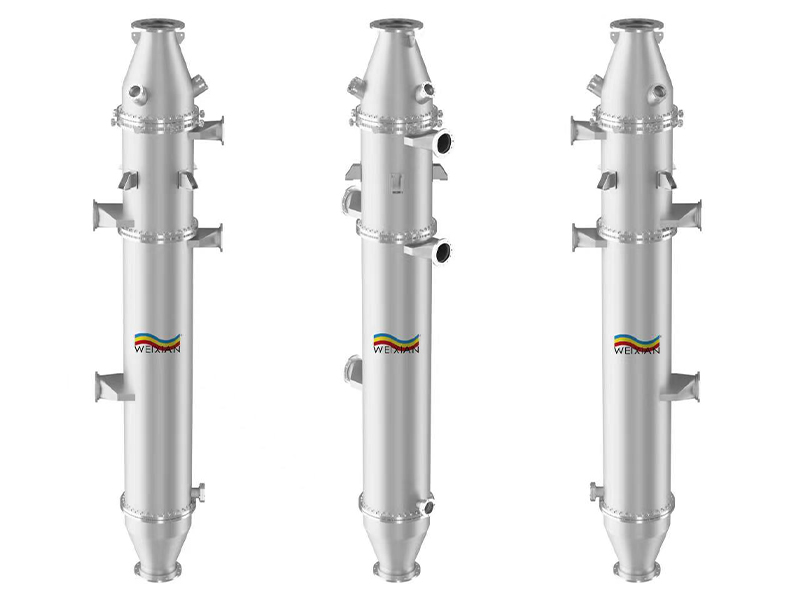
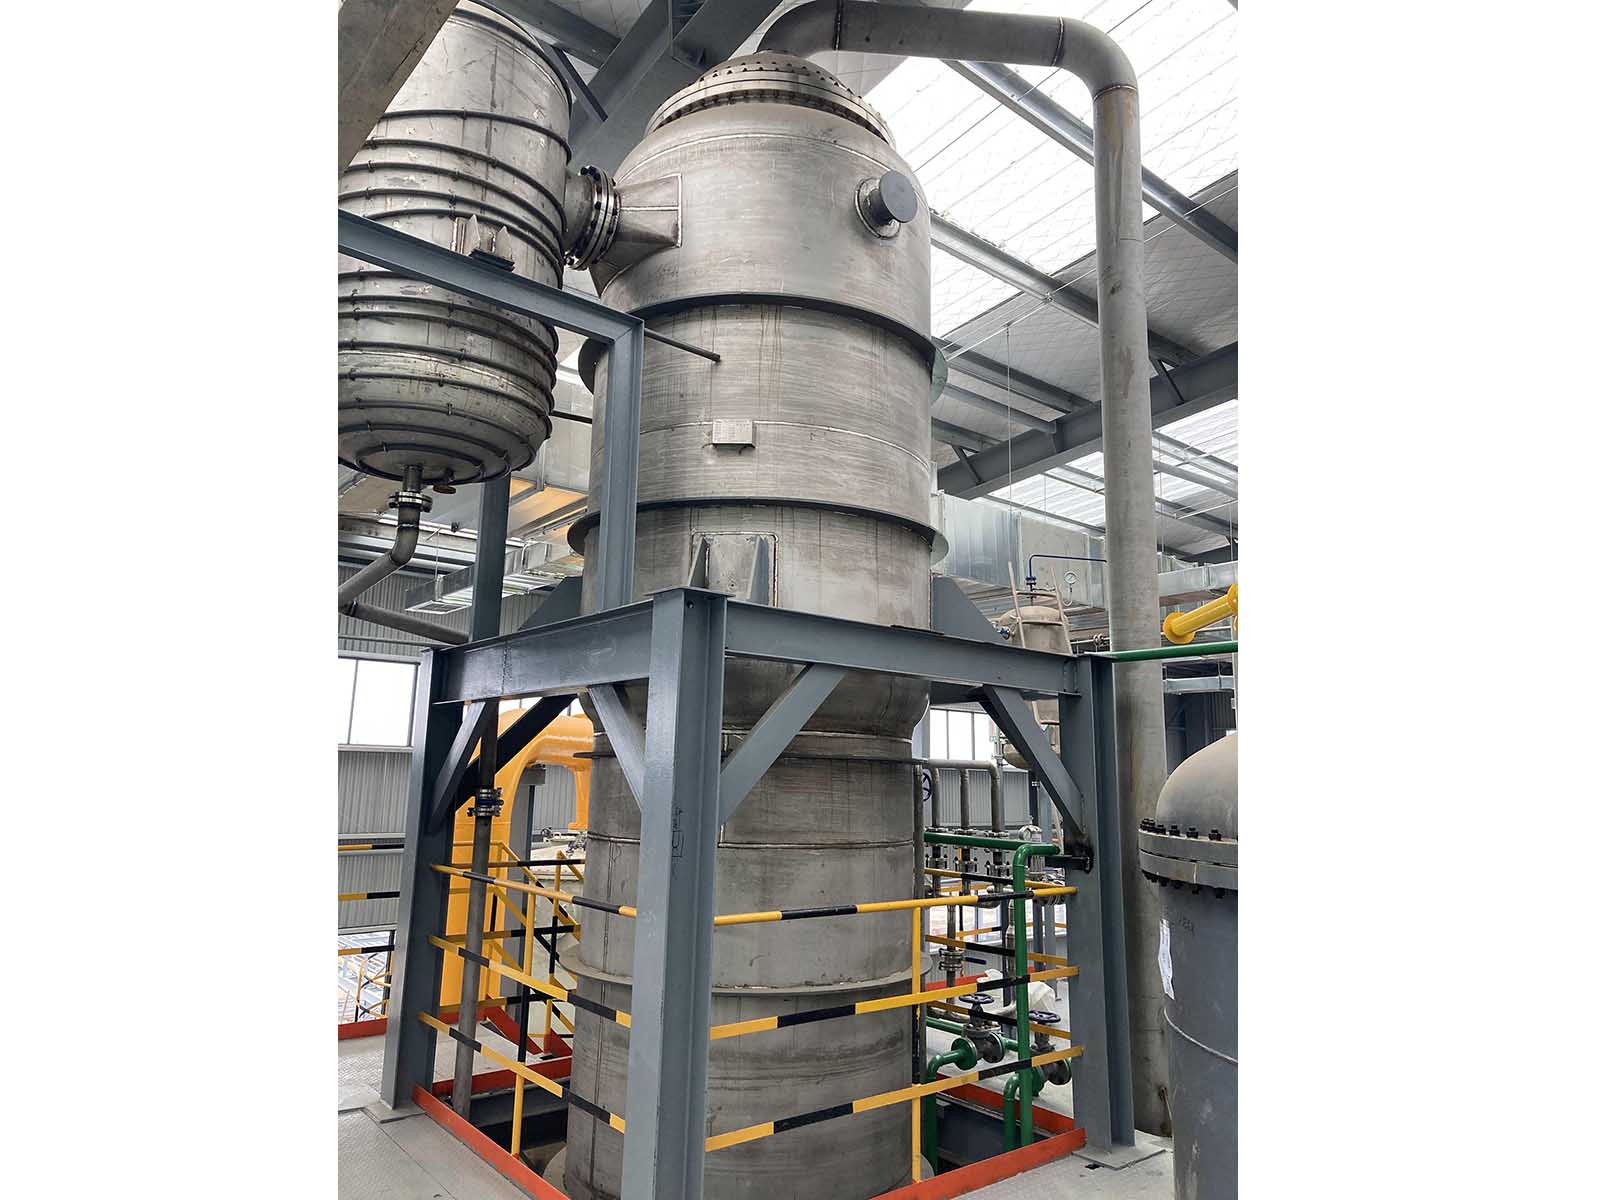
WEIXIAN adopts multi-tube falling film reactor. Its capacity ranges from single-tube configuration up to a 240-tube unit (10 t/h). Since 1995, WEIXIAN has delivered hundreds of reactors, among which more than 40 units feature a capacity exceeding 5 t/h. By 2026, WEIXIAN had successfully commissioned six set of 7.5 or 8t/h reactors.
1. Organic feed distribution system at reactor head
After calibration, flow deviation is controlled within ±1.5%. The distribution header and nozzles are machined and formed in a single clamping setup via CNC machining. Critical dimensional tolerances are guaranteed at ±0.005 mm, with secondary dimensions held to ±0.01 mm.
2. Surface finish of reaction tube inner bore
Reaction tubes are manufactured by high-precision cold rolling followed by annealing, and treated under vacuum at 1040 °C to eliminate intermolecular residual stress. These processes yield an internal and external surface finish of Ra 0.4 (mirror-like) for each tube; the inner and outer diameter deviation of reaction tubes is limited to less than ±0.02 mm.
3. Welding and non-destructive inspection for distribution header and reaction tubes
The joint between distribution header and reaction tube employs high-frequency welding combined with GTAW (gas tungsten arc welding, argon arc welding), with fillet weld geometry. Non-destructive testing (NDT) is adopted for flaw detection. Every individual tube undergoes a 0.6 MPa hydrostatic pressure test and endoscopic inspection to verify weld integrity and internal tube dimensional accuracy.
4. Concentricity of the three tube sheets
All three tube sheets are machined on a machining center using a unified coordinate system. Tube concentricity tolerance is ±0.01 mm. The three tube sheets are stacked and secured in their assembly orientation, then every hole is checked one by one using an inspection mandrel to confirm concentricity deviation ≤ ±0.01 mm.
5. Sealing reliability
5.1 Cooling water seal between upper shell section and middle/lower shell sections
Cooling water flows into the second and third shell sections and discharges from the third section of the sulfonator. The first (upper) section is strictly isolated to maintain a separate circulation of 15 °C chilled water. This is critical to superior product quality, particularly for AOS production.
5.2 Bidirectional sealing for SO₃ and organic feed at the sulfonator upper section
On the first tube sheet, the compression screw assembly uses a composite screw head plus triple combined gaskets to form robust bidirectional sealing. It achieves complete isolation from oleum and prevents corrosion and leakage.
5.3 Cooling water sealing between distribution header and shell side
An innovative sealing structure significantly improves shell-side pressure resistance. The shell-side test pressure exceeds 0.6 MPa, permitting pressurized water return. All sealing elements are special fluororubber O-rings, delivering 100% sealing performance with lifetime maintenance-free operation.
5.4 Cooling water sealing at the lower reaction tube and shell side
Fluororubber O-rings are implemented here, providing 100% sealing performance and lifetime maintenance-free operation.
6. Additional technical advantages of WEIXIAN sulfonator
6.1 Extended operating campaign: Continuous LABSA production campaign ≥40 days
6.2 Continuous production campaign for 70% SLES exceeds 3 months
6.3 Continuous production campaign for AOS ≥25 days
6.4 Convenient sulfonator calibration Flow deviation at initial start-up can be controlled within ±1.5%. Replacement gaskets are available in thicknesses of 1.8–2.2 mm (standard thickness: 2 mm). This ensures premium product quality and extends sulfonator cleaning intervals.
6.5 Production turndown flexibility
LABSA capacity adjustment range: 55%–115%
70% SLES capacity adjustment range: 80%–140%
It adopts the cathode plate hollow-out design to avoid “black acid” accumulation. Cathode SS wires are replaced by SS tubes, in order to eliminate the risk of breaking.
The working voltage is 40,000 V, featured in excellent SO3 and organic acid mists removal performance.
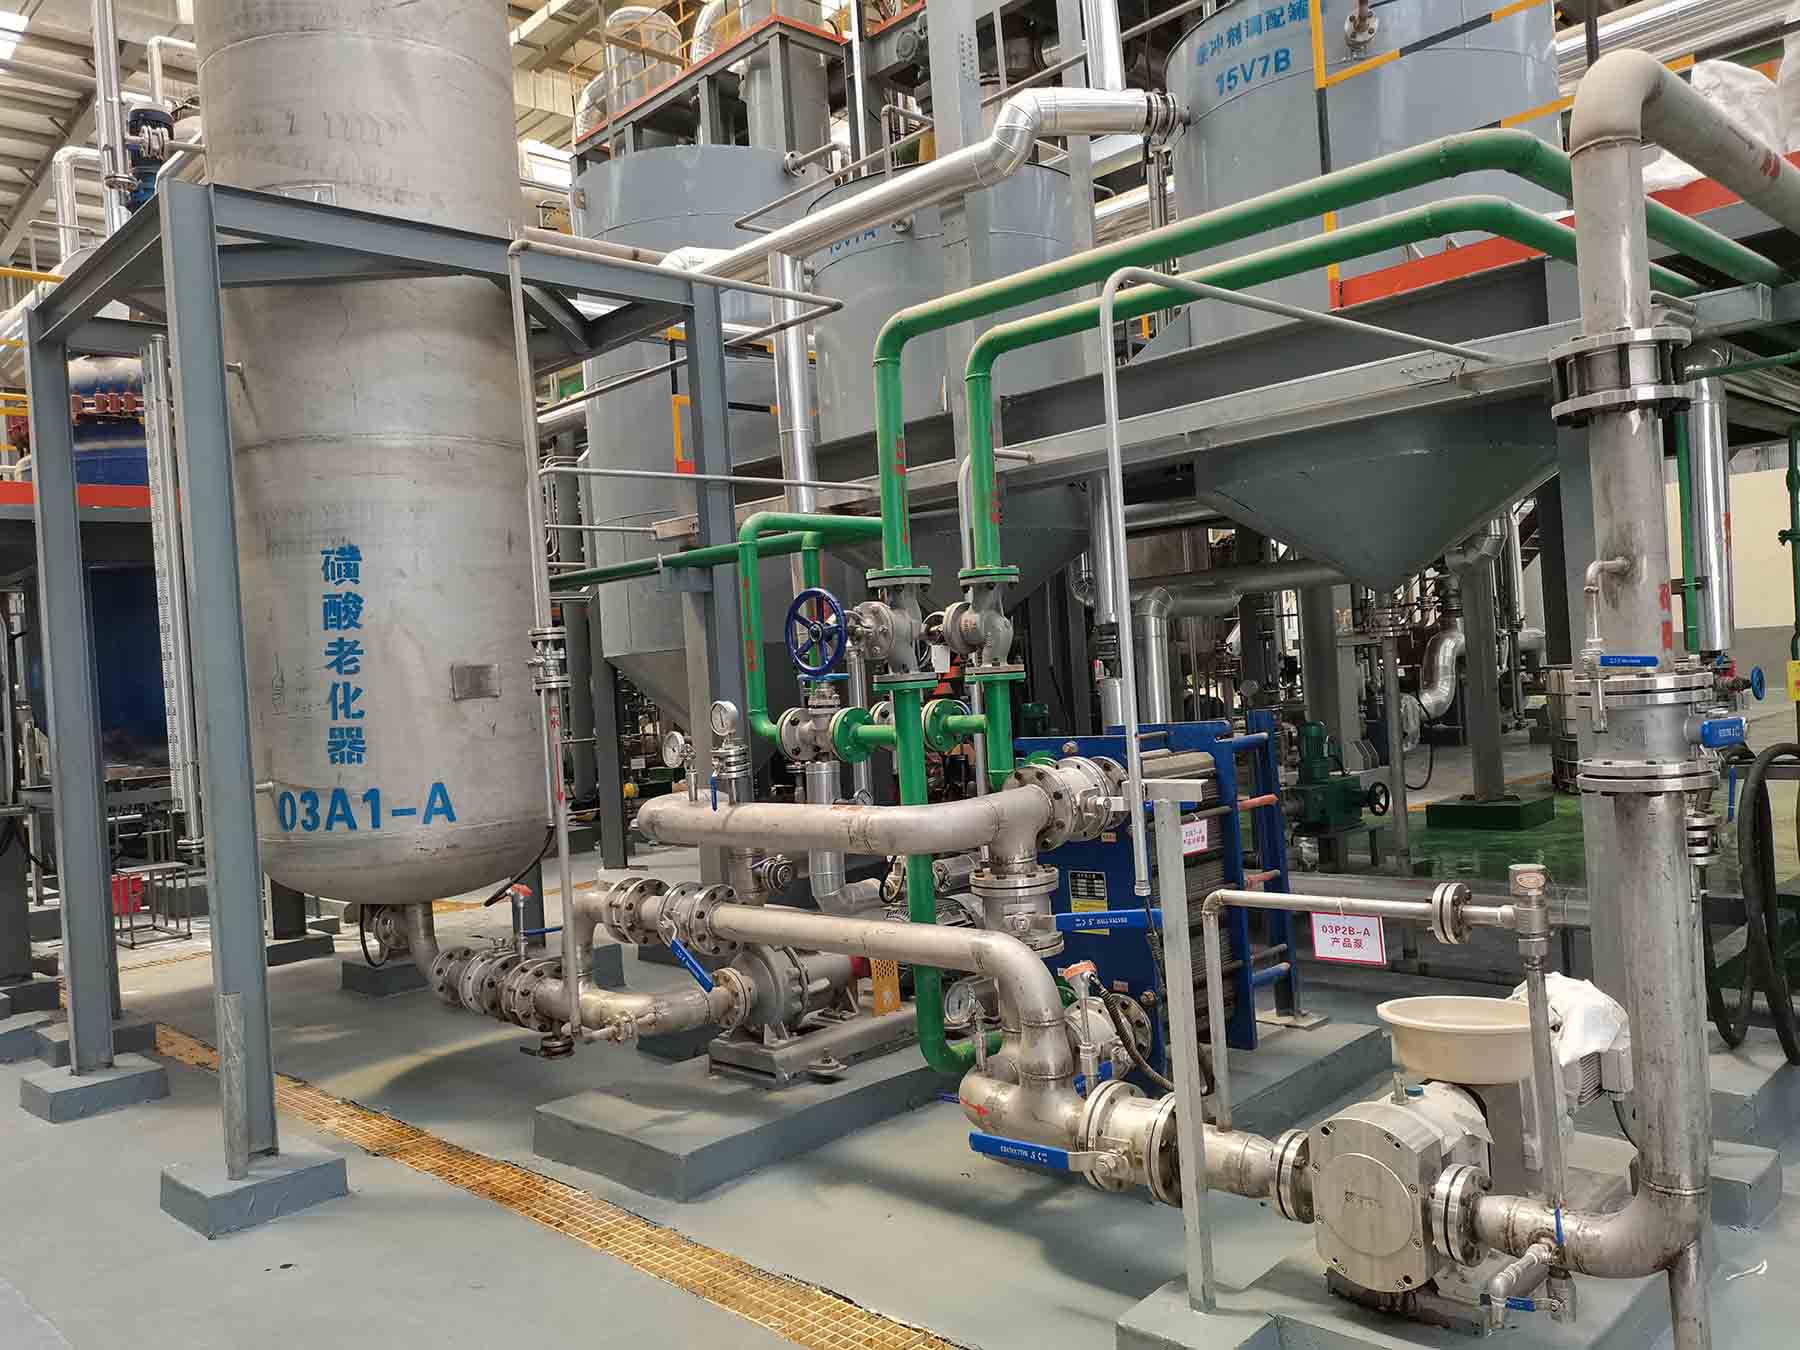
Unlike conventional agitated rotary aging vessels, our static unit provides a more homogeneous aging effect and eliminates back-mixing.
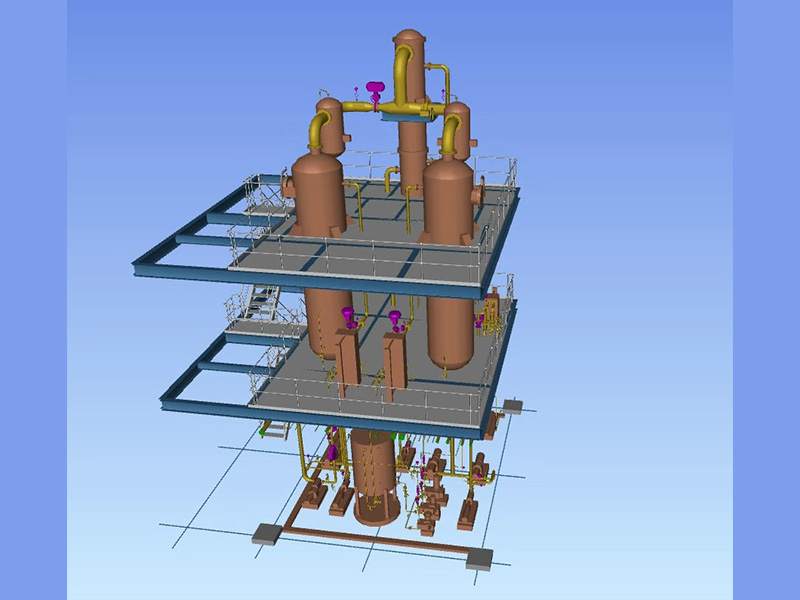
Equipped with proprietary internals, the static aging vessel ensures uniform residence time for all material molecules. In contrast, molecules in rotary aging vessels have non-uniform residence time following a normal distribution. The aging duration is adjustable from 0 to 60 minutes by regulating the liquid level inside the vessel. Typically, the aging time is set at 30 minutes. Where higher active matter content is required, e.g., for LABSA with active matter of 97.5%–98%, the aging time may be set to 45–60 minutes. In addition to superior process performance, this static equipment features lower power consumption and reduced maintenance demand.
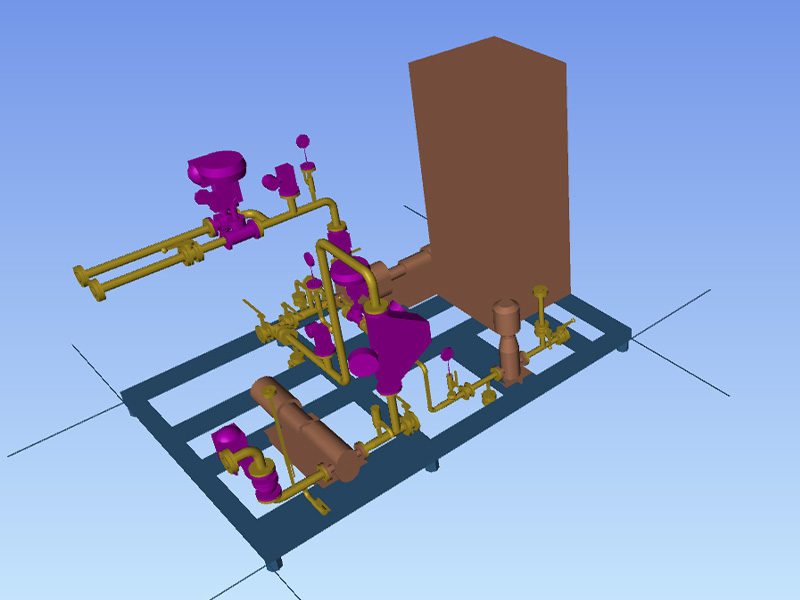
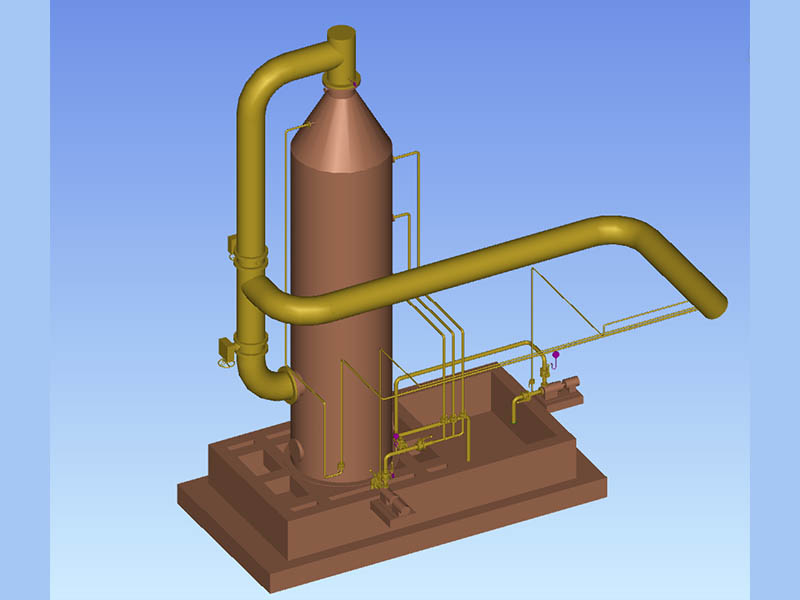
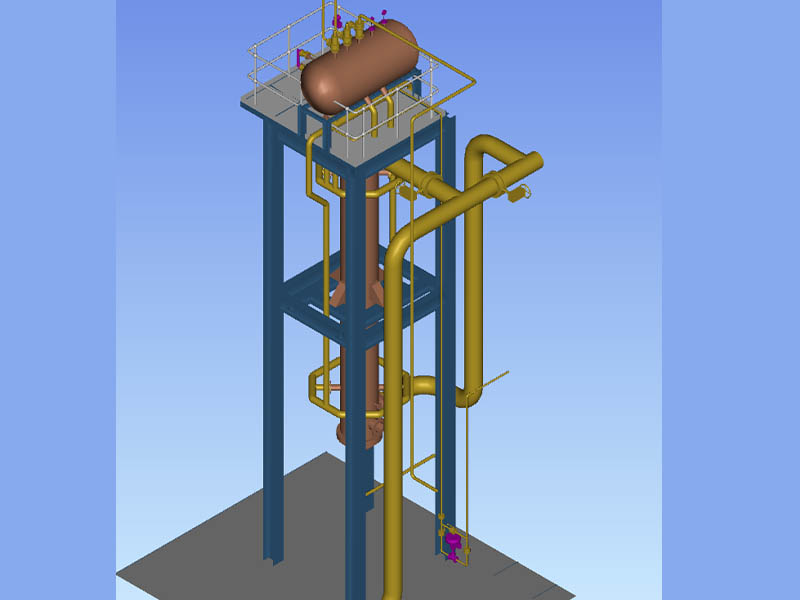
Stripping tower 79T1 is static equipment, without motor or rotating parts. Compared to outdated technology, our stripping tower doesn’t need maintenance. WEIXIAN designs the stripping tower based on the characteristic of sulfonated/sulphonated products. In the stripping tower, degassing, water removal, dioxane stripping, and cooling can be achieved in the same equipment, which can save power consumption, and ensure stable running and product quality.
The high-shear neutralization reactor consists of multiple high-speed dispersing-shearing discs. Its mechanical seals and bearings are custom-designed for high-speed mixing and shearing service, enabling stable operation at 960 rpm.
This neutralization reactor features efficient and homogeneous mixing, flexible operation, stable system pressure and low failure rate.
The converter adopts a vertical SS304 stainless steel packed tower structure with a maximum temperature resistance of 700°C.
It delivers stable conversion efficiency, flexible operational adjustment and precise temperature control, and achieves maintenance-free operation. The tower is configured with four packing layers filled with V₂O₅ composite catalysts combining low-temperature and medium-temperature catalytic formulations. This design not only realizes a low light-off temperature but also ensures an SO₂ conversion rate of over 98%. It significantly improves start-up preheating efficiency and reduces preheating duration.
Dedicated thermometer interfaces are reserved at the top and bottom of each catalyst bed to support accurate temperature regulation and sustain high conversion efficiency. Each bed is equipped with a manhole to facilitate on-site catalyst loading and replacement.
The heat-pipe heat exchanger features high heat transfer efficiency, compact structural layout and low flue-side flow resistance. With inherently safe and reliable structural characteristics, it outperforms conventional heat exchangers of other types. Damage to individual or a small number of heat pipes will not impair overall equipment performance or interrupt plant production. Since the water circuit is arranged externally to the flue gas duct, component replacement and routine overhaul can be performed without plant shutdown.
The equipment offers a design service life of over 10 years. Matched with the start-up preheater, the system can generate steam during cold start-up, eliminating the need for external steam supply.
Waste heat recovery performance is quantified as follows: 250 kg of steam is generated per 100 kg of sulfur combustion. The primary and secondary flue gas waste heat recovery stages produce steam, while the tertiary stage yields hot water, with corresponding heat recovery efficiencies of 36.5%, 44.2% and 67.3% respectively.
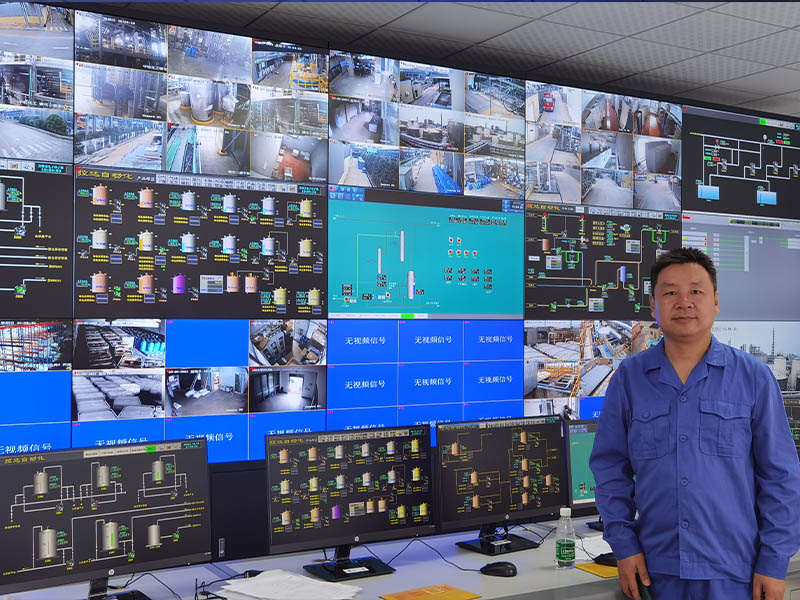
The control system adopts mainstream industrial brands including Siemens, ABB, Supcon, Hollysys, Honeywell or equivalent alternatives.
Field instruments are supplied by internationally renowned manufacturers: Emerson for mass flow meters, Michell for dew point meters, Mettler Toledo for pH meters, and Yokogawa for transmitters. Major electrical components are sourced from world-class brands such as Siemens, Schneider and ABB.
The entire plant is designed for high-level fully automatic operation. All programming and system configuration are completed by our in-house technical team. Remote parameter adjustment is available with the client’s authorization.
WEIXIAN adopts multi-tube falling film reactor. Its capacity ranges from single-tube configuration up to a 240-tube unit (10 t/h). Since 1995, WEIXIAN has delivered hundreds of reactors, among which more than 40 units feature a capacity exceeding 5 t/h. By 2026, WEIXIAN had successfully commissioned six set of 7.5 or 8t/h reactors.
1. Organic feed distribution system at reactor head
After calibration, flow deviation is controlled within ±1.5%. The distribution header and nozzles are machined and formed in a single clamping setup via CNC machining. Critical dimensional tolerances are guaranteed at ±0.005 mm, with secondary dimensions held to ±0.01 mm.
2. Surface finish of reaction tube inner bore
Reaction tubes are manufactured by high-precision cold rolling followed by annealing, and treated under vacuum at 1040 °C to eliminate intermolecular residual stress. These processes yield an internal and external surface finish of Ra 0.4 (mirror-like) for each tube; the inner and outer diameter deviation of reaction tubes is limited to less than ±0.02 mm.
3. Welding and non-destructive inspection for distribution header and reaction tubes
The joint between distribution header and reaction tube employs high-frequency welding combined with GTAW (gas tungsten arc welding, argon arc welding), with fillet weld geometry. Non-destructive testing (NDT) is adopted for flaw detection. Every individual tube undergoes a 0.6 MPa hydrostatic pressure test and endoscopic inspection to verify weld integrity and internal tube dimensional accuracy.
4. Concentricity of the three tube sheets
All three tube sheets are machined on a machining center using a unified coordinate system. Tube concentricity tolerance is ±0.01 mm. The three tube sheets are stacked and secured in their assembly orientation, then every hole is checked one by one using an inspection mandrel to confirm concentricity deviation ≤ ±0.01 mm.
5. Sealing reliability
5.1 Cooling water seal between upper shell section and middle/lower shell sections
Cooling water flows into the second and third shell sections and discharges from the third section of the sulfonator. The first (upper) section is strictly isolated to maintain a separate circulation of 15 °C chilled water. This is critical to superior product quality, particularly for AOS production.
5.2 Bidirectional sealing for SO₃ and organic feed at the sulfonator upper section
On the first tube sheet, the compression screw assembly uses a composite screw head plus triple combined gaskets to form robust bidirectional sealing. It achieves complete isolation from oleum and prevents corrosion and leakage.
5.3 Cooling water sealing between distribution header and shell side
An innovative sealing structure significantly improves shell-side pressure resistance. The shell-side test pressure exceeds 0.6 MPa, permitting pressurized water return. All sealing elements are special fluororubber O-rings, delivering 100% sealing performance with lifetime maintenance-free operation.
5.4 Cooling water sealing at the lower reaction tube and shell side
Fluororubber O-rings are implemented here, providing 100% sealing performance and lifetime maintenance-free operation.
6. Additional technical advantages of WEIXIAN sulfonator
6.1 Extended operating campaign: Continuous LABSA production campaign ≥40 days
6.2 Continuous production campaign for 70% SLES exceeds 3 months
6.3 Continuous production campaign for AOS ≥25 days
6.4 Convenient sulfonator calibration Flow deviation at initial start-up can be controlled within ±1.5%. Replacement gaskets are available in thicknesses of 1.8–2.2 mm (standard thickness: 2 mm). This ensures premium product quality and extends sulfonator cleaning intervals.
6.5 Production turndown flexibility
LABSA capacity adjustment range: 55%–115%
70% SLES capacity adjustment range: 80%–140%
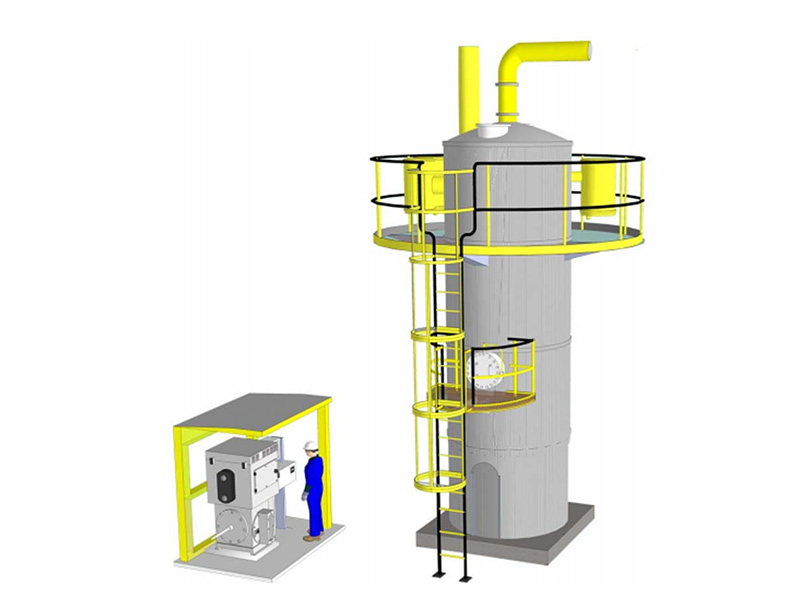
It adopts the cathode plate hollow-out design to avoid “black acid” accumulation. Cathode SS wires are replaced by SS tubes, in order to eliminate the risk of breaking.
The working voltage is 40,000 V, featured in excellent SO3 and organic acid mists removal performance.
Unlike conventional agitated rotary aging vessels, our static unit provides a more homogeneous aging effect and eliminates back-mixing.
Equipped with proprietary internals, the static aging vessel ensures uniform residence time for all material molecules. In contrast, molecules in rotary aging vessels have non-uniform residence time following a normal distribution. The aging duration is adjustable from 0 to 60 minutes by regulating the liquid level inside the vessel. Typically, the aging time is set at 30 minutes. Where higher active matter content is required, e.g., for LABSA with active matter of 97.5%–98%, the aging time may be set to 45–60 minutes. In addition to superior process performance, this static equipment features lower power consumption and reduced maintenance demand.
Stripping tower 79T1 is static equipment, without motor or rotating parts. Compared to outdated technology, our stripping tower doesn’t need maintenance. WEIXIAN designs the stripping tower based on the characteristic of sulfonated/sulphonated products. In the stripping tower, degassing, water removal, dioxane stripping, and cooling can be achieved in the same equipment, which can save power consumption, and ensure stable running and product quality.
The high-shear neutralization reactor consists of multiple high-speed dispersing-shearing discs. Its mechanical seals and bearings are custom-designed for high-speed mixing and shearing service, enabling stable operation at 960 rpm.
This neutralization reactor features efficient and homogeneous mixing, flexible operation, stable system pressure and low failure rate.
The converter adopts a vertical SS304 stainless steel packed tower structure with a maximum temperature resistance of 700°C.
It delivers stable conversion efficiency, flexible operational adjustment and precise temperature control, and achieves maintenance-free operation. The tower is configured with four packing layers filled with V₂O₅ composite catalysts combining low-temperature and medium-temperature catalytic formulations. This design not only realizes a low light-off temperature but also ensures an SO₂ conversion rate of over 98%. It significantly improves start-up preheating efficiency and reduces preheating duration.
Dedicated thermometer interfaces are reserved at the top and bottom of each catalyst bed to support accurate temperature regulation and sustain high conversion efficiency. Each bed is equipped with a manhole to facilitate on-site catalyst loading and replacement.
The heat-pipe heat exchanger features high heat transfer efficiency, compact structural layout and low flue-side flow resistance. With inherently safe and reliable structural characteristics, it outperforms conventional heat exchangers of other types. Damage to individual or a small number of heat pipes will not impair overall equipment performance or interrupt plant production. Since the water circuit is arranged externally to the flue gas duct, component replacement and routine overhaul can be performed without plant shutdown.
The equipment offers a design service life of over 10 years. Matched with the start-up preheater, the system can generate steam during cold start-up, eliminating the need for external steam supply.
Waste heat recovery performance is quantified as follows: 250 kg of steam is generated per 100 kg of sulfur combustion. The primary and secondary flue gas waste heat recovery stages produce steam, while the tertiary stage yields hot water, with corresponding heat recovery efficiencies of 36.5%, 44.2% and 67.3% respectively.
The control system adopts mainstream industrial brands including Siemens, ABB, Supcon, Hollysys, Honeywell or equivalent alternatives.
Field instruments are supplied by internationally renowned manufacturers: Emerson for mass flow meters, Michell for dew point meters, Mettler Toledo for pH meters, and Yokogawa for transmitters. Major electrical components are sourced from world-class brands such as Siemens, Schneider and ABB.
The entire plant is designed for high-level fully automatic operation. All programming and system configuration are completed by our in-house technical team. Remote parameter adjustment is available with the client’s authorization.
WEIXIAN is an engineering company specialized in supplying turnkey sulphonation/sulphation plant and it's technology, focusing on the R&D of LABSA, SLES, SLS, AOS, HABSA, MES and other anionic surfactant production technologies.