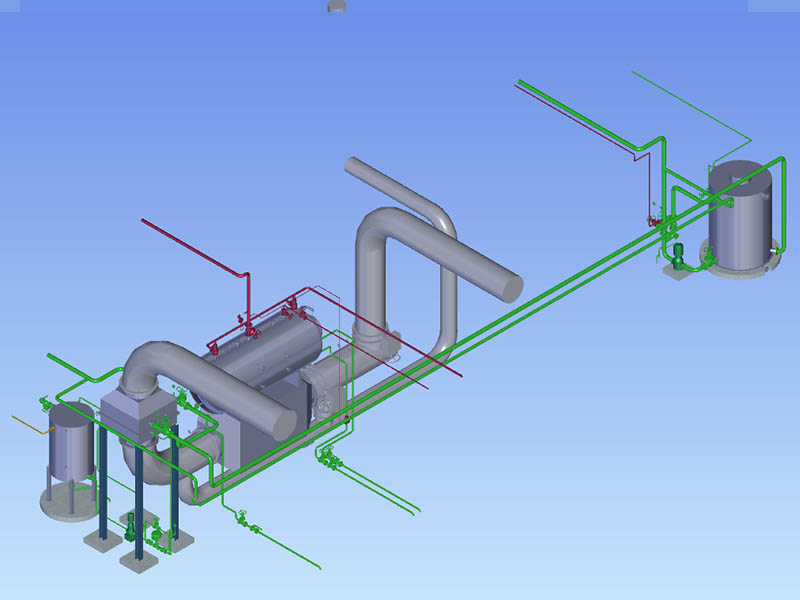
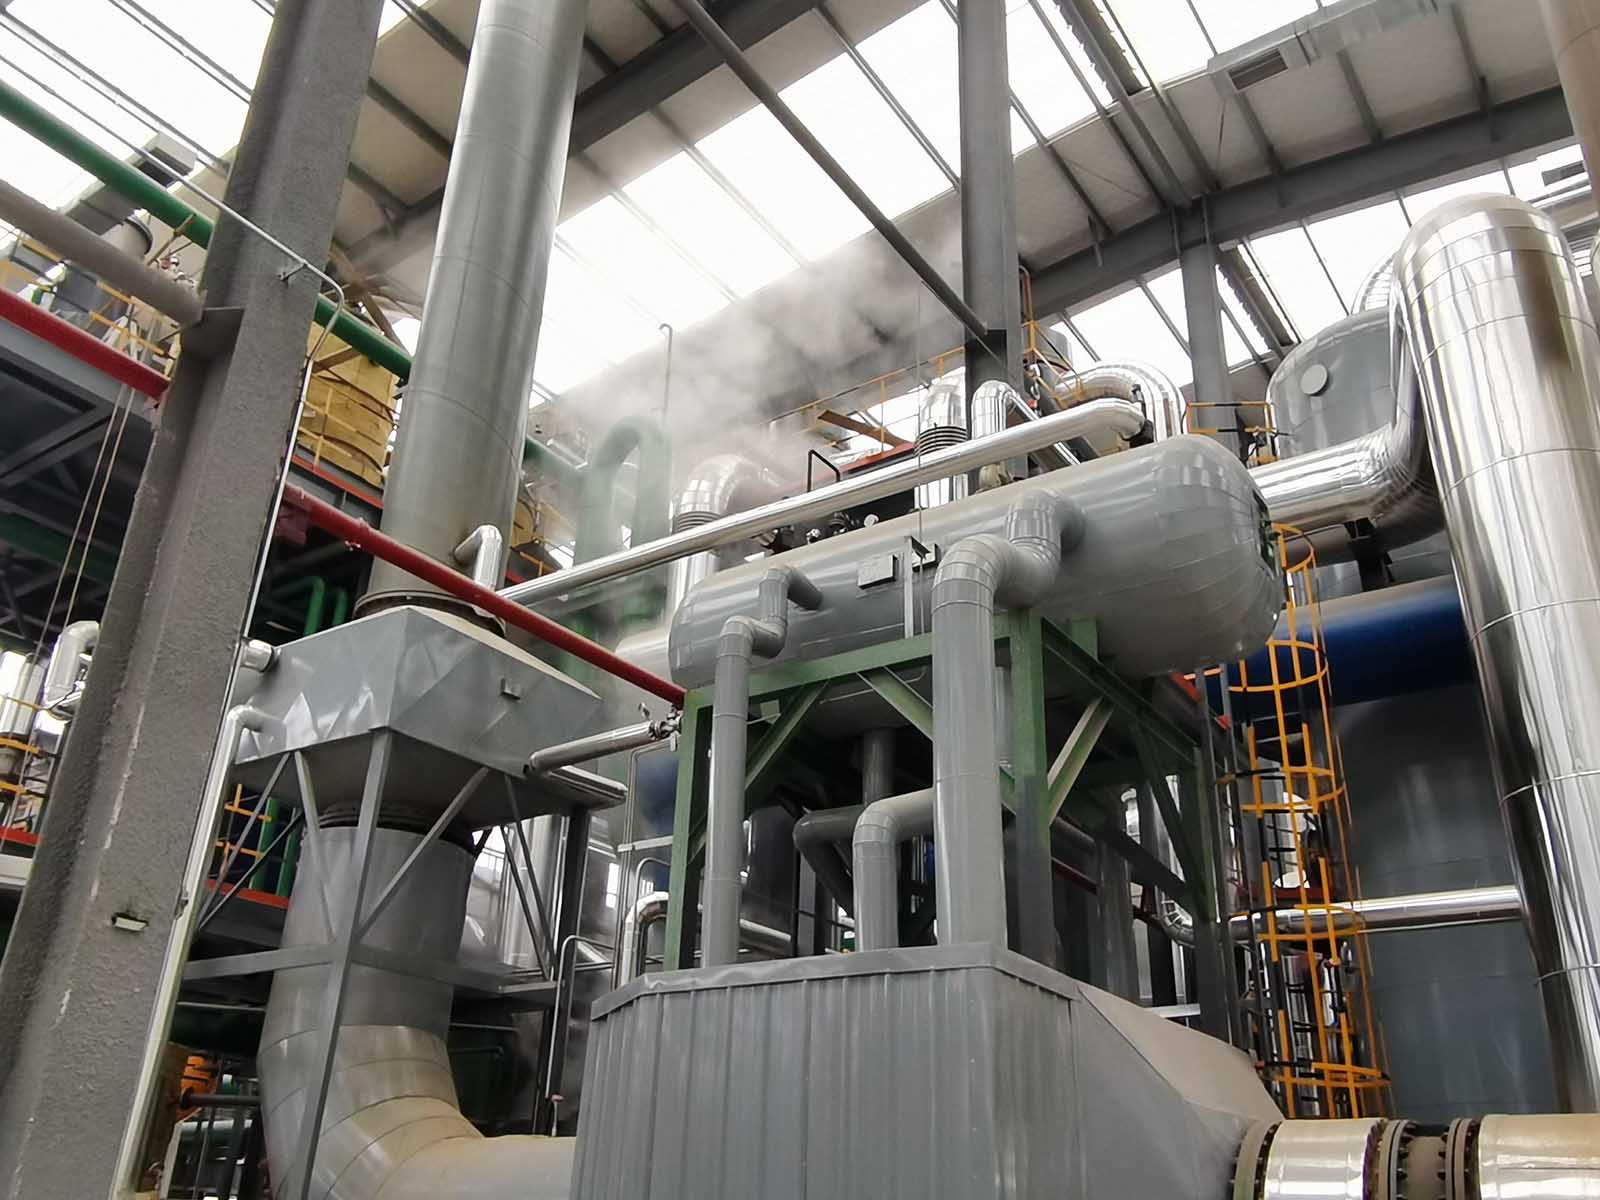
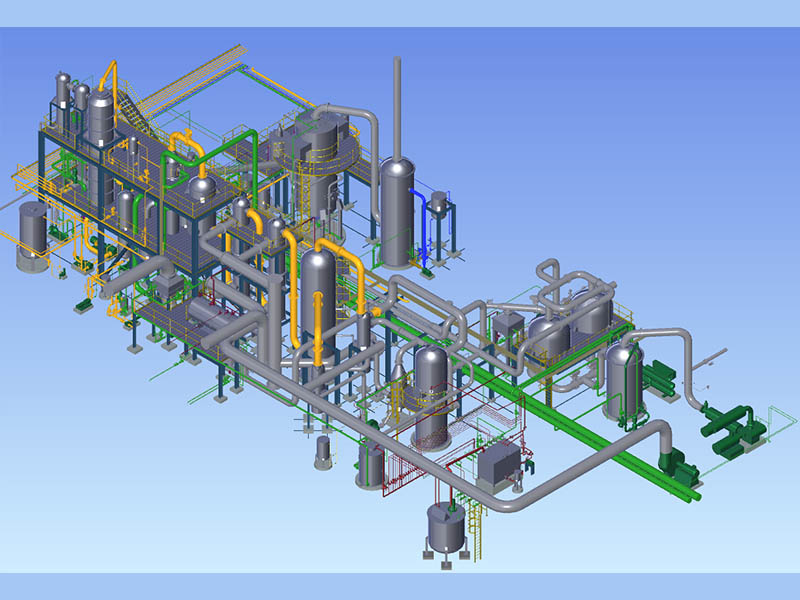
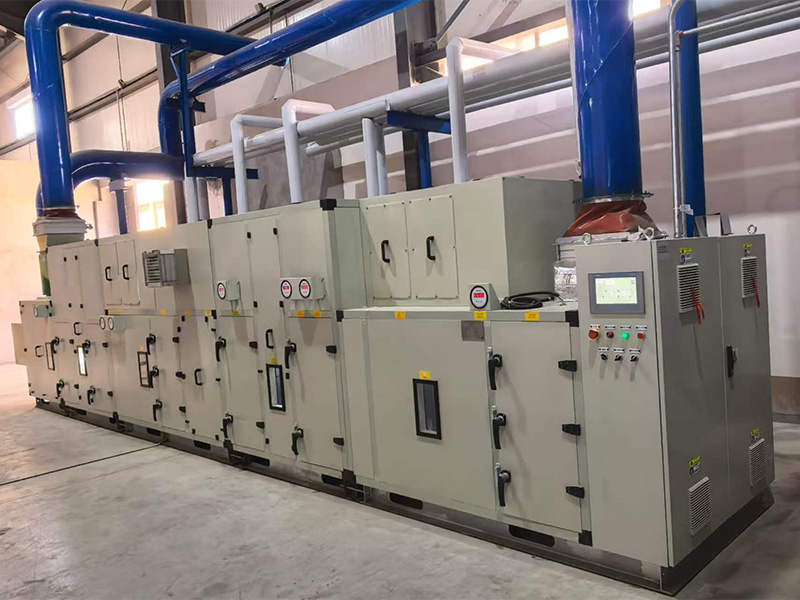
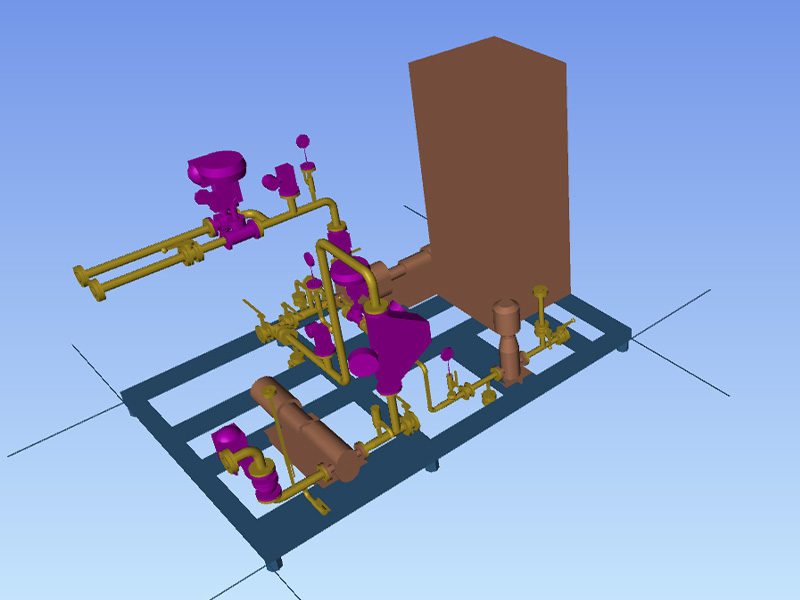
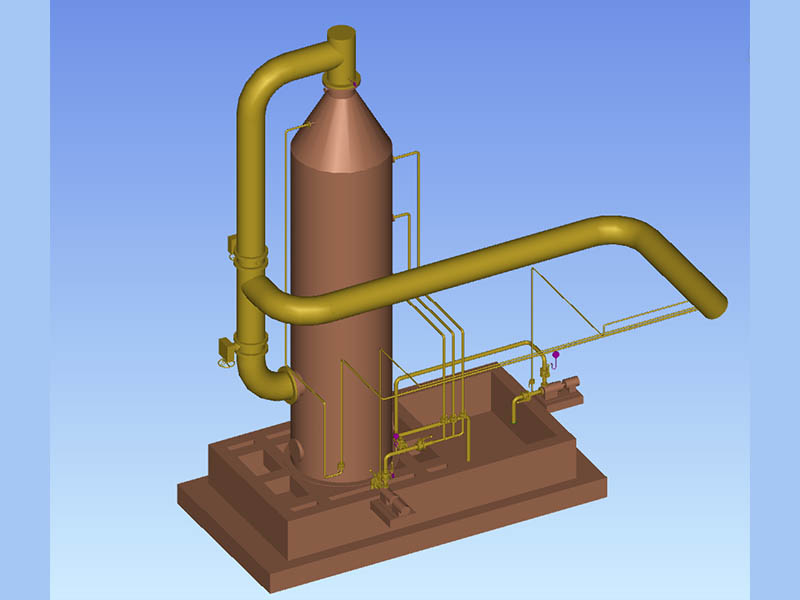
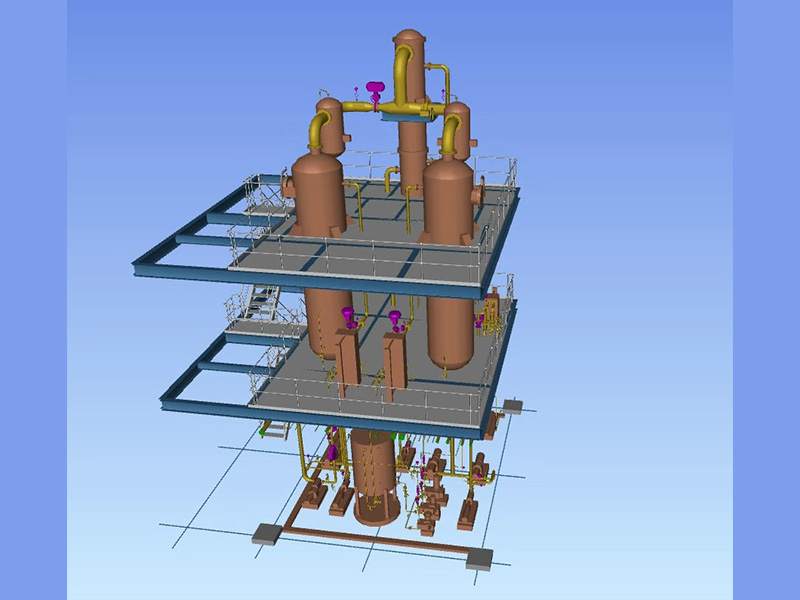
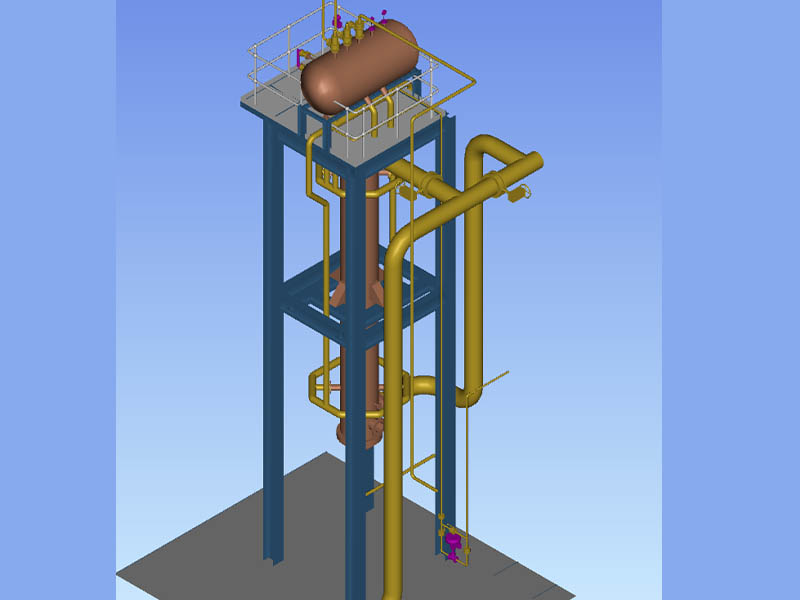
The hot air first enters the heat-pipe exchanger, where heat is transferred to the soft water inside, generating steam at 0.4–0.6 MPa. After leaving the heat-pipe exchanger, the hot air is further used to pre-heat the reverse-osmosis (R/O) water and produce hot water.
Features: With the waste heat recovery system, the plant requires no external steam for cold start-up. During normal operation, the plant achieves full steam and hot-water self-sufficiency.
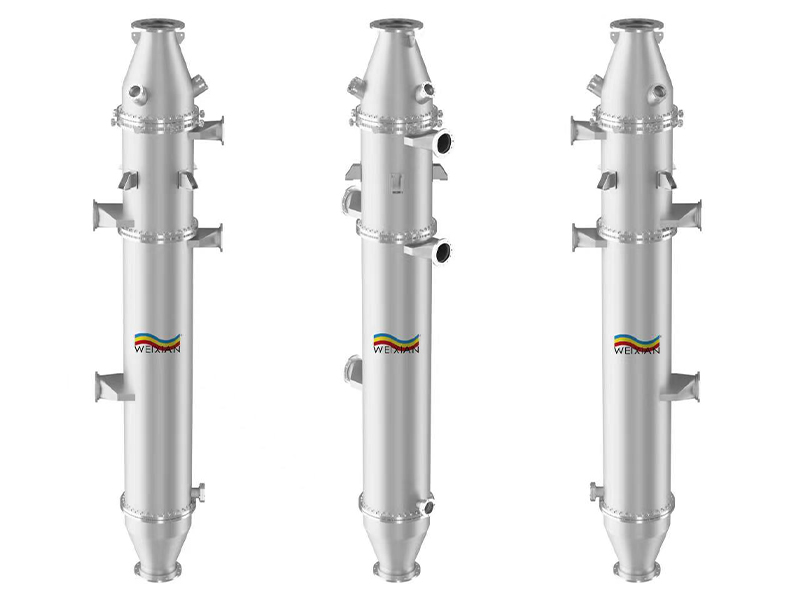
The heat-pipe heat exchanger features high heat transfer efficiency, compact structural layout and low flue-side flow resistance. With inherently safe and reliable structural characteristics, it outperforms conventional heat exchangers of other types. Damage to individual or a small number of heat pipes will not impair overall equipment performance or interrupt plant production. Since the water circuit is arranged externally to the flue gas duct, component replacement and routine overhaul can be performed without plant shutdown.
The equipment offers a design service life of over 10 years. Matched with the start-up preheater, the system can generate steam during cold start-up, eliminating the need for external steam supply.
Waste heat recovery performance is quantified as follows: 250 kg of steam is generated per 100 kg of sulfur combustion. The primary and secondary flue gas waste heat recovery stages produce steam, while the tertiary stage yields hot water, with corresponding heat recovery efficiencies of 36.5%, 44.2% and 67.3% respectively.
The hot air first enters the heat-pipe exchanger, where heat is transferred to the soft water inside, generating steam at 0.4–0.6 MPa. After leaving the heat-pipe exchanger, the hot air is further used to pre-heat the reverse-osmosis (R/O) water and produce hot water.
Features: With the waste heat recovery system, the plant requires no external steam for cold start-up. During normal operation, the plant achieves full steam and hot-water self-sufficiency.
The heat-pipe heat exchanger features high heat transfer efficiency, compact structural layout and low flue-side flow resistance. With inherently safe and reliable structural characteristics, it outperforms conventional heat exchangers of other types. Damage to individual or a small number of heat pipes will not impair overall equipment performance or interrupt plant production. Since the water circuit is arranged externally to the flue gas duct, component replacement and routine overhaul can be performed without plant shutdown.
The equipment offers a design service life of over 10 years. Matched with the start-up preheater, the system can generate steam during cold start-up, eliminating the need for external steam supply.
Waste heat recovery performance is quantified as follows: 250 kg of steam is generated per 100 kg of sulfur combustion. The primary and secondary flue gas waste heat recovery stages produce steam, while the tertiary stage yields hot water, with corresponding heat recovery efficiencies of 36.5%, 44.2% and 67.3% respectively.
WEIXIAN is an engineering company specialized in supplying turnkey sulphonation/sulphation plant and it's technology, focusing on the R&D of LABSA, SLES, SLS, AOS, HABSA, MES and other anionic surfactant production technologies.